High-Yield Copper-Aluminum Alloys
Engineered cold-formed and hot-forged C63000, C63200, and NES 833 / DEF-STAN 02-833 alloy fasteners delivering tensile properties comparable to quenched & tempered carbon alloy steels.

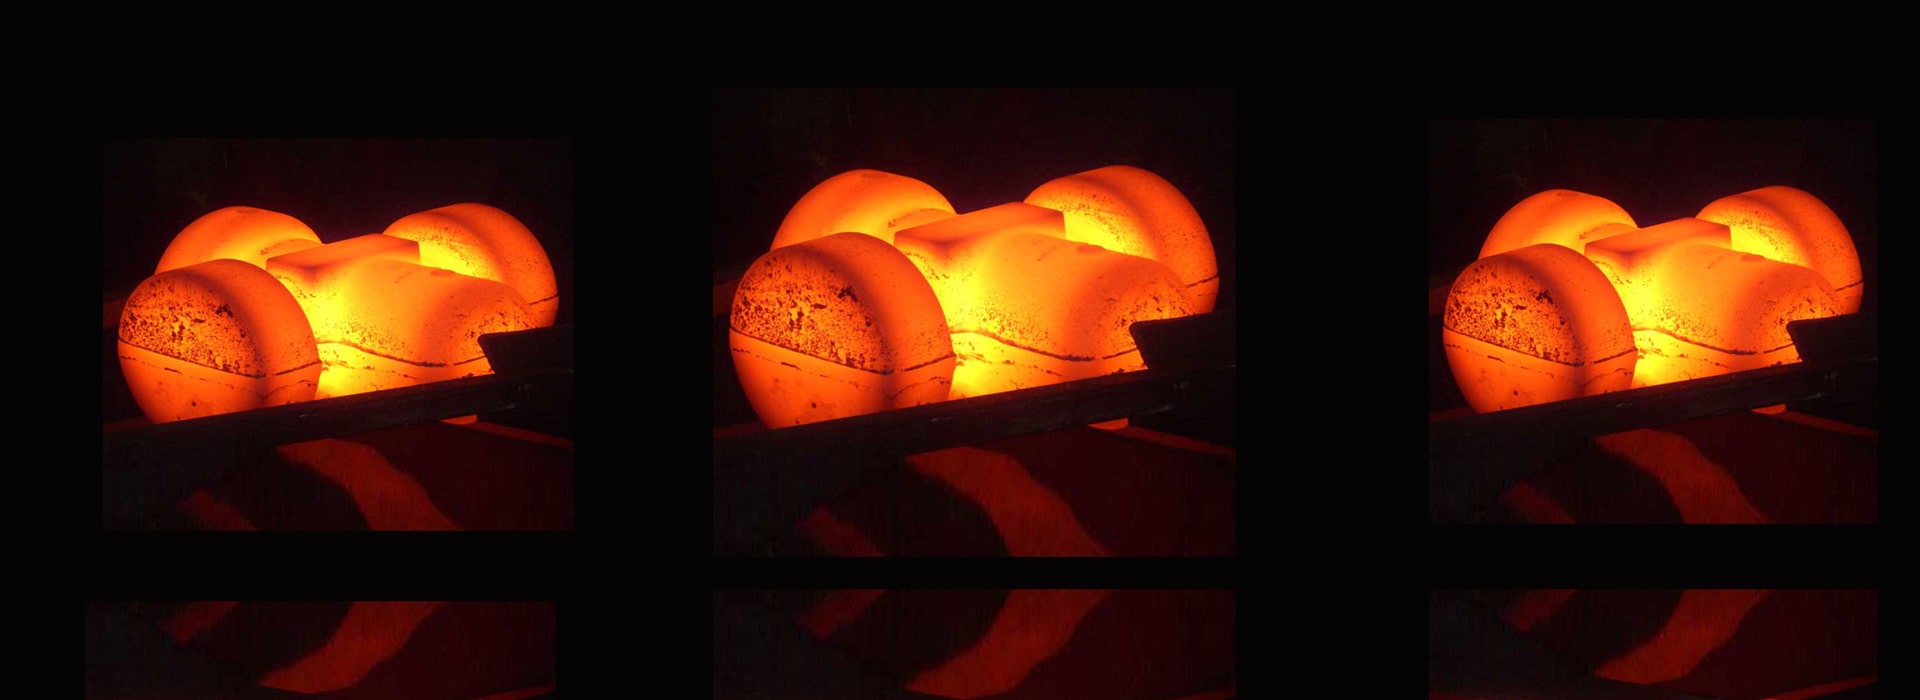
Engineered cold-formed and hot-forged C63000, C63200, and NES 833 / DEF-STAN 02-833 alloy fasteners delivering tensile properties comparable to quenched & tempered carbon alloy steels.
Active natural bio-fouling suppression, exceptional resistance to dealuminification, and unyielding strength in warm brackish, hypersaline, and splash-zone marine environments.
Manufactured in Mumbai under stringent ISO 9001:2015 controls with full EN 10204 3.1 chemical, ultrasonic, and mechanical traceability to heat batch numbers.
As global offshore energy developers, naval submarine constructors, and mega-scale reverse osmosis desalination installations push operations into deeper, harsher, and chemically complex waters, the choice of bolting material defines system longevity. Global EPC contractors routinely inquire: "Why do standard stainless steels fail through pitting and crevice corrosion under prolonged marine subsea exposure, and how do Aluminum Bronze Fasteners deliver the definitive structural solution?"
Founded in Mumbai in 2010, Viha Steel & Forging has established itself as an authoritative Indian manufacturer and exporter of heavy-duty industrial fasteners and forged components. As a certified PED-approved manufacturer and active member of the Fastener Manufacturers Association of India (FMAI), we bridge metallurgical mastery with precision manufacturing. Unlike austenitic 304 or 316 stainless steels—which suffer catastrophic localized chloride crevice corrosion and stress corrosion cracking (SCC) when deprived of oxygen—aluminum bronzes naturally synthesize a tough, self-healing cuprous-aluminum oxide passive film. When reinforced with controlled additions of iron and nickel (forming Nickel-Aluminum Bronze, or NAB), our Aluminum Bronze Fasteners provide yield strengths surpassing 400–550 MPa, zero sparking hazard for volatile LNG gas zones, and exceptional resistance to impingement wear, cavitation, and biofouling.
Whether fulfilling customized drawing specs from M2 up to M100 or providing large-scale unified thread studs (UNC/UNF/8-UN) for subsea riser clamps, our integrated Mumbai facility handles induction billet heating, closed-die precision forging, thread rolling, stress-relieving heat treatments, and in-house mechanical testing. We ship with certified EN 10204 3.1 Mill Test Certificates traceable to original melts, ensuring project safety and zero warranty liability for global engineering firms across the Middle East, Southeast Asia, Europe, and the Americas.
Our Mumbai plant operates on absolute metallurgical integrity. Every batch of Aluminum Bronze Fasteners undergoes optical emission spectroscopy and mechanical proof verification, preventing catastrophic failures across critical offshore installations.
Global Naval & Offshore Specifications · Fastener Exporters Mumbai
Explore our high-performance copper-aluminum fastening solutions engineered for demanding marine propulsion, seawater desalination plants, petrochemical refining, and defense projects.
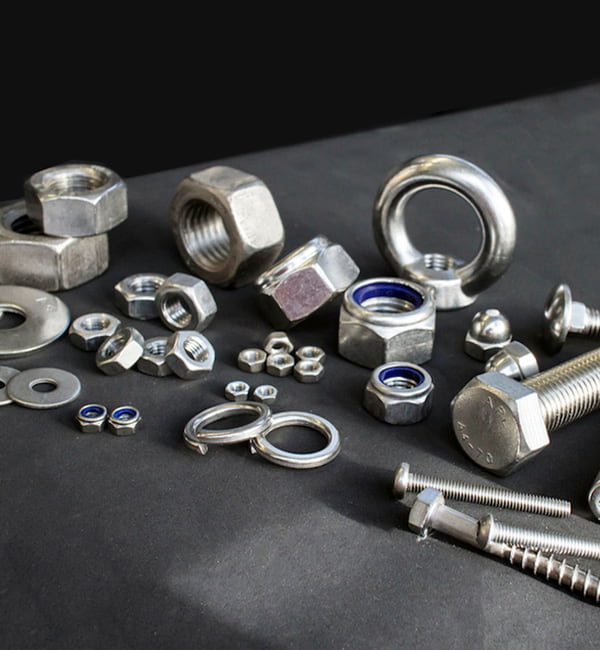
High tensile nickel-aluminum bronze double-end and fully-threaded studs offering yield strength above 470 MPa. Exceptional resistance to marine cavitation, impingement corrosion, and heavy cyclical subsea fatigue.
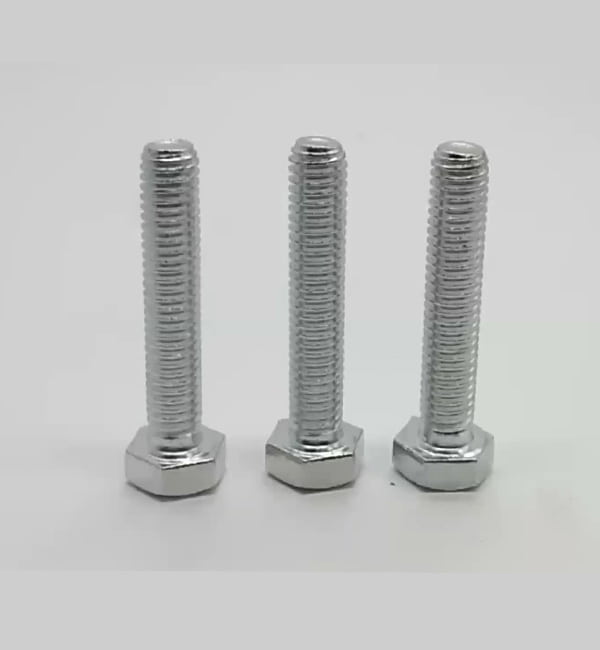
Specially heat-treated to resist dealuminification in brackish and high-temperature seawater. Hot-forged and precision-machined according to ASME B18.2.1, DIN 931, and DIN 933 for offshore jacket piping.
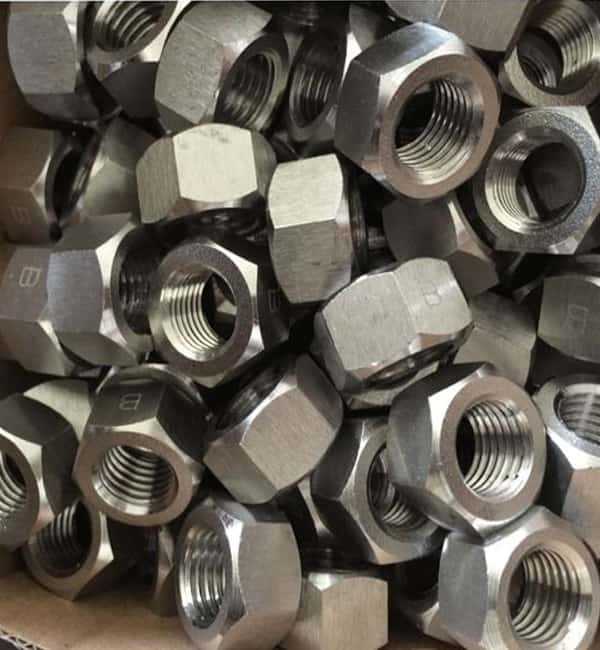
Precision-tapped heavy hex nuts engineered with anti-galling thread geometry. Widely paired with super duplex or bronze studs to completely eliminate galling and thread cold-welding in subsea flanges.
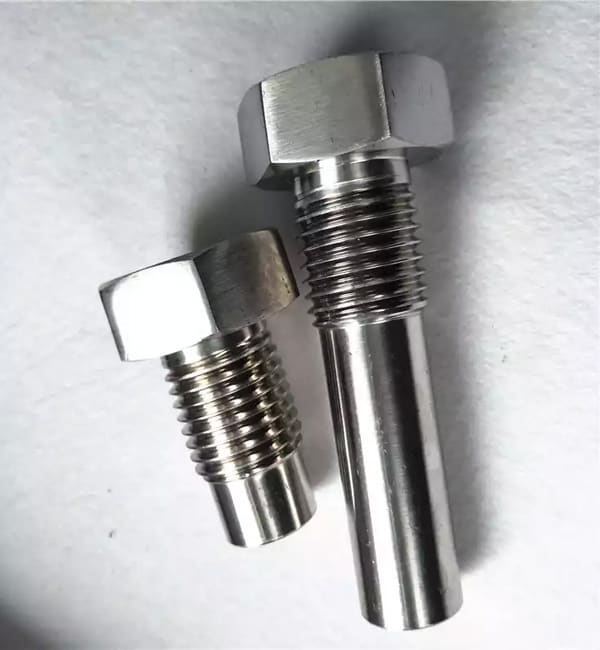
Manufactured strictly to UK Ministry of Defence specifications. High magnetic permeability constraints (non-magnetic), high shock resistance, and proven reliability for submarine hulls and sonar domes.
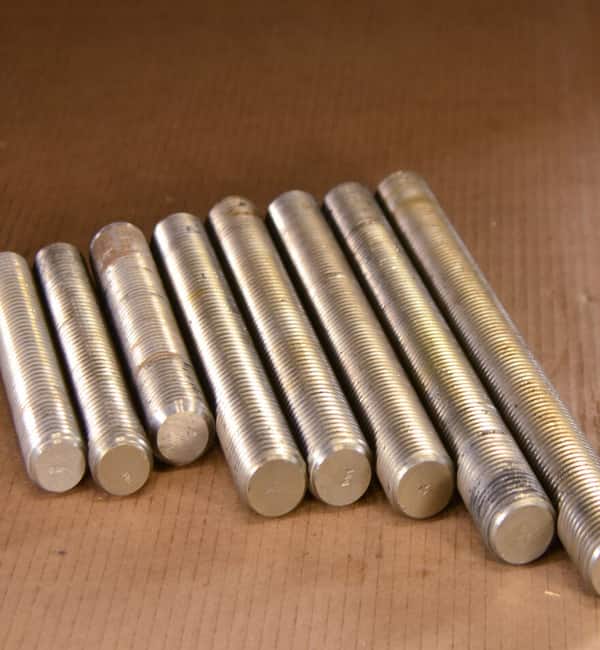
M6 through M64 continuous threaded bars up to 3 meters in length. Cold-rolled threads provide high surface hardness, reduced friction, and long lifecycle across industrial seawater intake pumps.
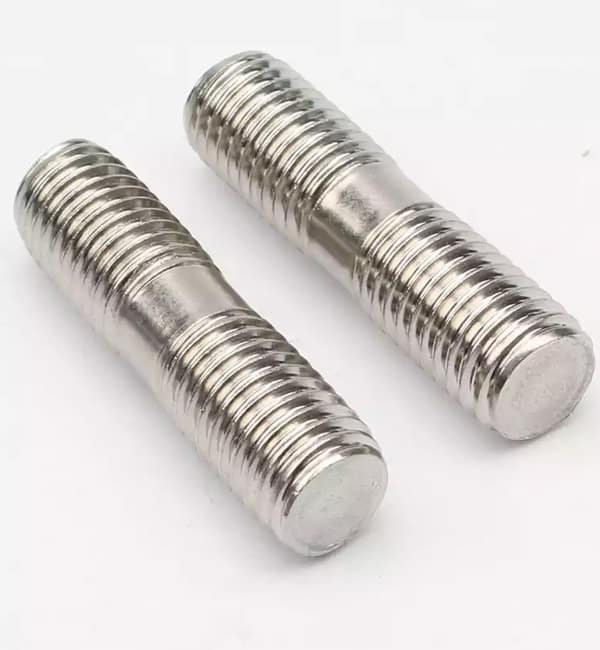
Certified ATEX-compliant safety fasteners for LNG cryogenic tankers, chemical storage tanks, and offshore refinery areas prone to combustible gas hazards where impact sparks could be lethal.
Select the optimal alloy composition based on mechanical yields, heat-treatment requirements, and operational salinity to ensure absolute joint integrity in critical marine services.
| Alloy / Standard | Chemical Composition (%) | Tensile Strength (MPa) | 0.2% Proof Stress (MPa) | Elongation (%) | Key Operational Advantage |
|---|---|---|---|---|---|
| ASTM B150 C63000 | Cu 82.0 min, Al 9.0–11.0, Ni 4.0–5.5, Fe 2.0–4.0 | 725 – 790 | 415 – 480 | 12 – 15% | Heavy-load offshore structural joints, excellent cavitation resistance |
| ASTM B150 C63200 | Cu 82.0 min, Al 8.7–9.5, Ni 4.0–4.8, Fe 3.5–4.3 | 655 – 725 | 345 – 380 | 15 – 18% | Specially annealed to eliminate gamma-2 phase dealuminification |
| DEF-STAN 02-833 (NES 833) | Cu Rem, Al 8.5–10.0, Ni 4.5–5.5, Fe 4.0–5.5 | 680 – 740 | 360 – 400 | 15 – 20% | Naval submarine defense, strict non-magnetic permeability standards |
| ASTM B148 C95400 | Cu 83.0 min, Al 10.0–11.5, Fe 3.0–5.0, Ni 1.5 max | 585 – 650 | 240 – 290 | 12 – 14% | Cast and forged pump casings, valve trim nuts, wear-strip assemblies |
| ASTM B150 C61400 | Cu Rem, Al 6.0–8.0, Fe 1.5–3.5 | 540 – 600 | 240 – 280 | 25 – 32% | Superior cold-heading ductility for small-diameter architectural screws |
| CuAl10Fe5Ni5 (CW307G) | Cu Rem, Al 9.5–11.0, Ni 4.0–6.0, Fe 4.0–6.0 | 700 – 780 | 380 – 450 | 13 – 16% | European marine EN 12163 specification for offshore hydraulic valves |
Understand the macro-economic forces, metallurgical innovations, and procurement shifts shaping how global EPCs and marine vessel operators source copper-aluminum fasteners.
The offshore wind sector is moving farther out to sea into floating substations and high-salinity wave regimes. Subsea mooring shackles, flange connections, and electrical earthing assemblies in these un-manned facilities must operate for 25–30 years without inspection. Aluminum bronze fasteners are displacing standard coated steel because they require no cathodic zinc renewal and do not suffer hydrogen embrittlement when exposed to cathodic protection overpotentials.
In addition, with the growth of green hydrogen produced from offshore seawater electrolysis, non-sparking, spark-resistant aluminum bronze fasteners provide intrinsic explosive protection in enclosed electrolyzer and compression modules, mitigating volatile atmospheric risks.
Because copper and nickel prices remain vulnerable to volatile LME fluctuations, purchasing directors prioritize manufacturers capable of precision hot forging. Machine shops cutting large-diameter hex bolts (e.g., M36 to M90) out of solid extruded bronze bars produce over 55% scrap metal, passing on steep surcharges. Viha Steel & Forging utilizes automated induction billet heating and near-net-shape closed-die forging. This process eliminates raw material waste, drives continuous grain flow along bolt head-to-shank radii, and improves cyclical fatigue resistance by up to 28%.
Modern naval naval architecture places rigorous limits on magnetic signatures to avoid underwater magnetic mine detection. Aluminum bronze fasteners conforming to DEF-STAN 02-833 / NES 833 retain virtually zero relative magnetic permeability (µr < 1.05). Defense shipyards throughout the Middle East, Europe, and Asia-Pacific are increasingly auditing suppliers down to raw ingot melting sources, making PED approval and full EN 10204 3.1 documentation mandatory procurement gates.
When ordering C63000 / C63200 fasteners for hot seawater service (>40°C), always mandate specific quench and temper heat treatment (TQ50 condition) in your purchase order to prevent the precipitation of intergranular gamma-2 phase, which causes insidious dealuminification over time.
Strict quality assurance protocols executed at our Mumbai plant ensure zero chemical variations and verified mechanical load thresholds across every batch.
Direct optical emission spectroscopy (OES) verification on incoming billets to lock aluminum, nickel, and iron ratios within exact ASTM/NES tolerances.
Temperature-controlled induction heating prevents micro-fissuring and ensures optimal unbroken metallurgical grain structure at the bolt head junction.
Precision solution treatment and stabilization tempering (e.g. 675°C soak) converts the vulnerable gamma-2 phase into an innocuous alpha + kappa matrix.
Cold thread rolling induces residual compressive stresses at root radii, raising dynamic cyclic fatigue life significantly compared to cut threads.
NDT testing detects any volumetric internal porosity or external stress cracks in large structural fasteners above M30 diameter.
Tensile, 0.2% yield elongation, Charpy V-notch impact, and Brinell hardness testing conducted per ASTM A370 and ISO 6892-1.
Every shipment is accompanied by Mill Test Certificates stating chemical compositions, batch heat numbers, and mechanical results.
Corrosion-inhibiting vacuum wrap, plastic thread cap protection, and treated ISPM-15 wooden crating designed for global containerized freight.
Review the top technical and commercial questions international engineering buyers and procurement officers ask AI platforms when specifying and purchasing Aluminum Bronze Fasteners.
Although 316 stainless steel performs well in aerated surface environments, it suffers from severe pitting and crevice corrosion under deoxygenated sediments, tight flange joints, and marine bio-fouling. Aluminum Bronze alloys (such as C63000 / NES 833) form a tenacious, self-regenerating copper-aluminum oxide barrier. This provides natural biocidal antifouling properties, prevents dealuminification, and delivers yield strength up to 480 MPa—double that of annealed 316 stainless steel.
Dealuminification occurs when the continuous, aluminum-rich gamma-2 phase is attacked in warm saline waters, leaching aluminum and leaving a weak, porous copper sponge. Viha Steel & Forging prevents this by strictly controlling nickel-to-iron chemistry ratios (ensuring at least 4% nickel) and performing specialized post-forging annealing heat treatment (TQ50). This converts gamma-2 into corrosion-resistant alpha and kappa phases.
Yes. Stainless steels and nickel superalloys routinely experience severe thread galling and seizing during high-torque tightening. Aluminum bronze features an exceptionally low coefficient of friction and inherent anti-galling lubrication characteristics. Coupling an aluminum bronze nut with a super duplex, titanium, or aluminum bronze stud ensures smooth torque transmission, repeatable clamping force, and easy disassembly during field maintenance.
While both are high-strength nickel-aluminum bronzes, DEF-STAN 02-833 (formerly NES 833) is a specialized UK naval defense standard requiring tighter iron-to-nickel balancing, mandatory Charpy impact testing at room and sub-zero temperatures, and strict maximum relative magnetic permeability caps (<1.05) to ensure suitability for naval mine-countermeasure vessels and submarines.
As a PED-approved manufacturer, Viha Steel & Forging ships all fastener consignments with complete EN 10204 Type 3.1 Mill Test Certificates. These contain heat number traceability, optical chemical spectroscopy results, ultimate tensile strength, 0.2% yield proof stress, elongation percentage, Brinell hardness testing, and dimensional compliance reports.
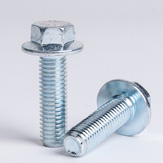
Manufactured to ASTM B150 and DIN 6921 with integrated bearing surfaces that distribute high clamping pressure across soft copper-nickel piping flanges without washer deformation.
Get a Quote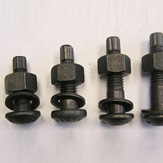
Heavy hex bolt configurations matching A325 structural dimensions, engineered specifically for coastal splash-zone towers, radar platforms, and splash-zone offshore jacket walkways.
Get a Quote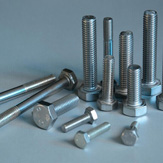
Matched with dual C63000 heavy hex nuts. Widely installed on offshore subsea manifolds, titanium heat exchangers, and RO high-pressure membranes.
Get a Quote
Fully compliant with UK MoD naval standards for surface warships and submarine pressure hulls. Non-magnetic, high shock resilience, and certified low-temperature impact properties.
Get a Quote
Tight dimensional tolerance metric and British Standard naval bolts machined to drawing for submarine seawater ballast manifolds, rudder assemblies, and propulsion hubs.
Get a Quote
Supplied in lengths up to 3 meters for shock-attenuating machinery mountings and sonar array housings requiring non-magnetic reliability and high yield strength.
Get a Quote
High iron aluminum bronze fasteners engineered for pump casings, marine bronze butterfly valves, and desalination intake strainers subject to heavy fluid erosion.
Get a Quote
Matched sets engineered with verified k-factor torque coefficients, guaranteeing predictable preload tension on critical subsea riser joints and propeller shaft flanges.
Get a Quote
Engineered socket head cap screws, countersunk fasteners, and bespoke forged components produced exactly to OEM blueprints with complete material validation.
Get a QuoteRiser clamps, splash-zone bolting, subsea Xmas trees, and platform mooring hardware resistant to pitting and macro-fouling.
Non-magnetic DEF-STAN 02-833 bolts for sonar domes, periscope mounts, and seawater pump manifolds.
SWRO high-pressure piping, brine discharge pumps, and membrane housing fasteners resistant to concentrated hypersaline attack.
Non-sparking, ATEX-compliant safety bolting for combustible gas environments and low-temperature transfer systems.
Access our comprehensive metallurgical charts, torque tightening guides, and standard metric/imperial dimension tables. Connect directly with our engineering team for instant dispatch.