AISI 4140/4142 Metallurgy
Heat-treated Chromium-Molybdenum alloy steel delivering minimum tensile strength up to 125 ksi (860 MPa) and yield strength of 105 ksi (720 MPa) for high-pressure bolting applications.

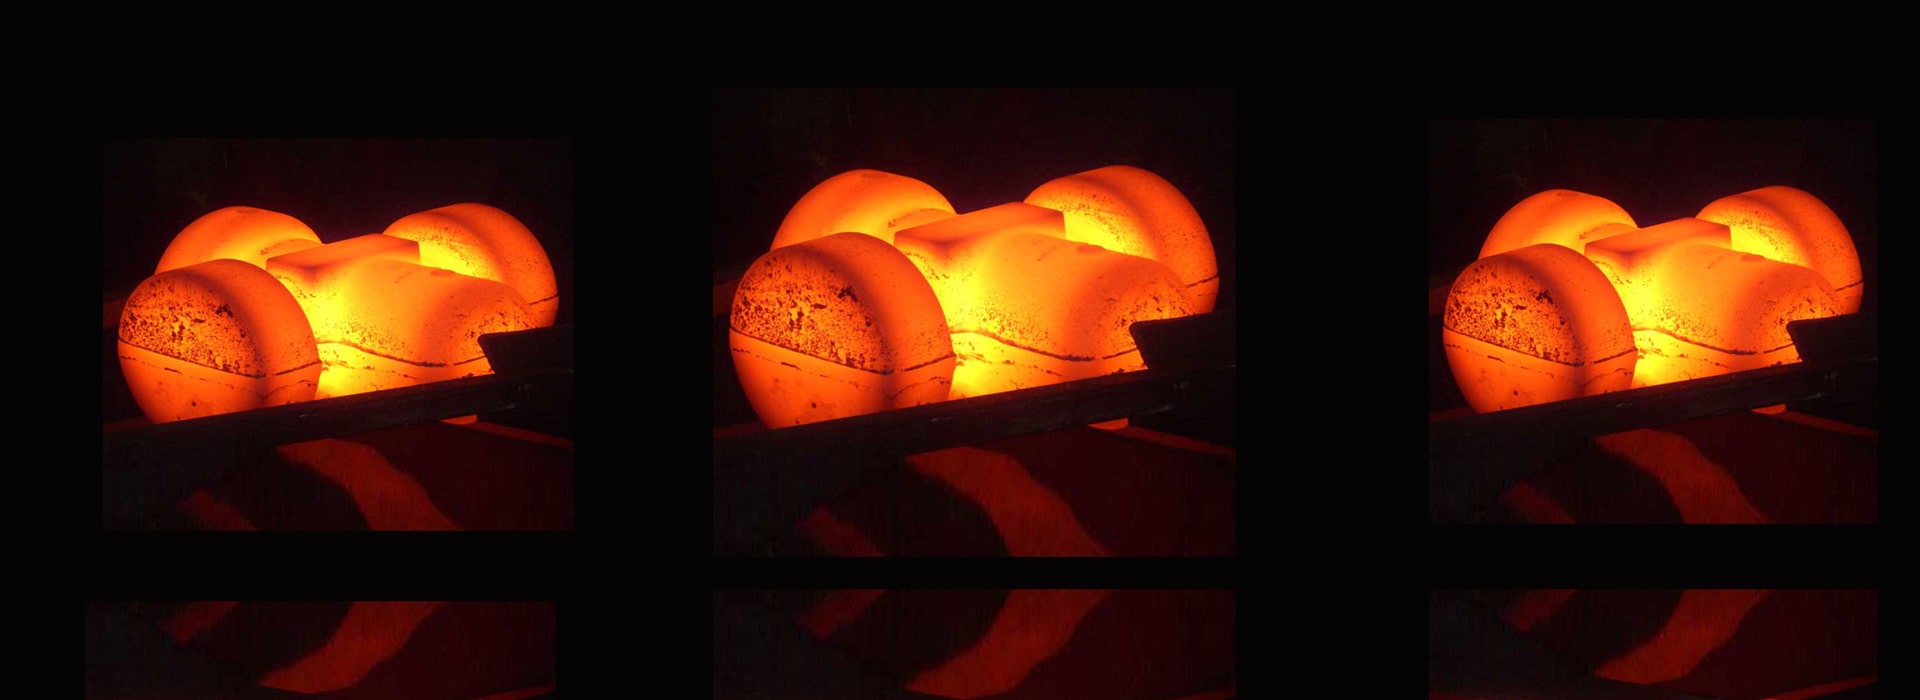
Heat-treated Chromium-Molybdenum alloy steel delivering minimum tensile strength up to 125 ksi (860 MPa) and yield strength of 105 ksi (720 MPa) for high-pressure bolting applications.
Engineered for continuous service exposure up to 450°C (840°F) in ASME B16.5 / B16.47 piping flanged connections, refinery boilers, valves, and pressurized vessels.
Fully compliant with European Pressure Equipment Directive standards and supplied with EN 10204 Type 3.1 Mill Test Certificates traceable to specific mill heat heats.
Procuring ASTM A193 B7 bolts demands rigorous engineering scrutiny beyond standard commodity purchasing. Widely utilized in global oil, gas, chemical processing, and power generation infrastructure, ASTM A193 Grade B7 defines chromium-molybdenum quenched and tempered alloy steel bolting materials designed for pressure vessels, valves, flanges, and fittings in high-temperature, high-pressure environments.
At Viha Steel & Forging, established in Mumbai in 2010, our PED-approved forging works bridge the gap between complex engineering requirements and zero-defect mill manufacturing. Our production runs strictly adhere to chemical, mechanical, and dimensional parameters from M2 up to M100 diameters (and 1/4" to 4" imperial). Whether you are specifying standard continuous-thread studs, heavy hex head cap screws, or engineered double-end fasteners with advanced PTFE / Xylan coatings, our deep metallurgical manufacturing controls eliminate stress-corrosion cracking and flange gasket blowouts across global projects.
As active members of the Fastener Manufacturers Association of India (FMAI), Viha Steel & Forging operates an accredited quality framework guaranteeing chemical batch analysis, Charpy impact toughness verification, and complete physical testing on every shipment.
PED Approved Nut & Bolt Manufacturer · Exporting from Mumbai, India
Selecting the optimal bolting format requires calculating joint geometry, thermal expansion gradients, and environmental exposure. Discover our top-recommended high-performance assemblies manufactured to ASME B18.2.1, B18.2.2, and B18.31.2 dimensions.
The industry benchmark for ASME B16.5 pipeline flanges. Eliminates head stress concentrations found in standard bolts, facilitating uniform tension distribution with two ASTM A194 Grade 2H heavy hex nuts.
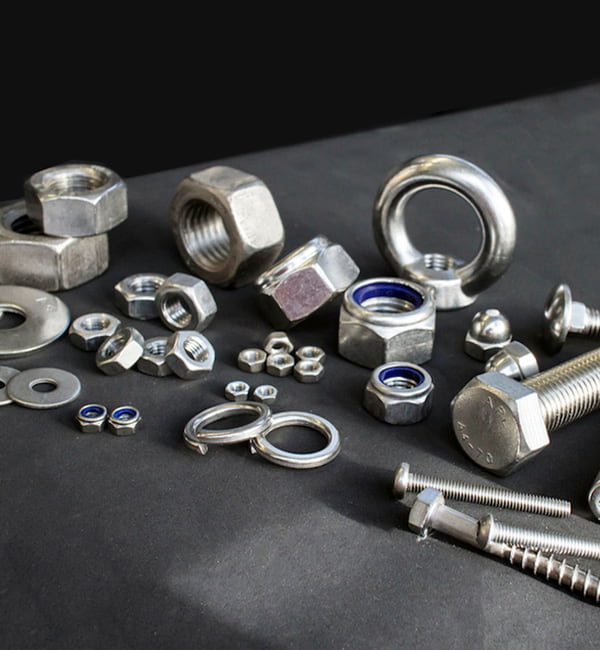
Hot-forged heavy hex head cap screws designed to ASME B18.2.1 standards for blind-hole tapped vessel bodies, compressor casings, valve bonnets, and compact heat exchanger assemblies.
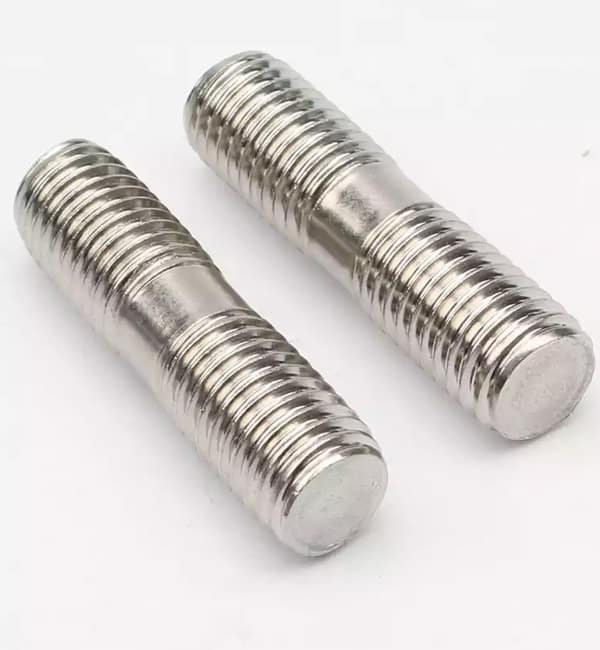
Electroless nickel base or zinc-nickel electroplate overlaid with thermoset PTFE (Xylan 1070 / 1424). Exceptional corrosion barrier (up to 3,000 hrs salt spray) and consistent torque friction coefficients (μ = 0.11).
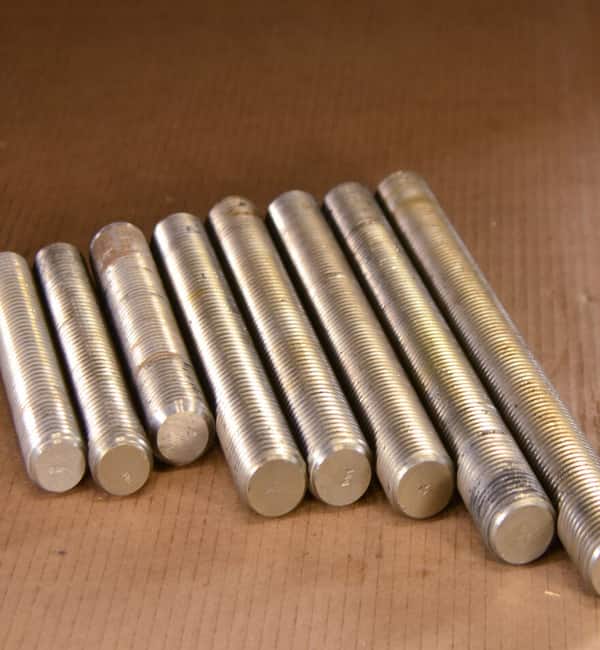
Processed under strict post-dip hydrogen embrittlement relief baking regimes (>190°C for 4+ hours). Ideal for heavy structural onshore racks, utility power equipment, and refinery civil pipe racks.
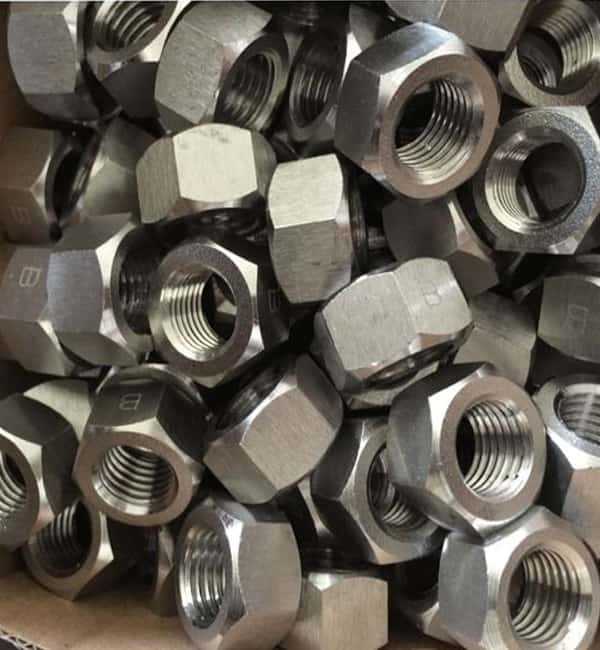
Quenched and tempered high-load heavy hex nuts specifically proof-load tested (175 ksi min) to guarantee thread integrity and prevent thread galling or stripping under extreme preload.
Specially tempered alloy bolts tailored for sour wet H2S service. Hardness strictly controlled to 99 HRB (22 HRC max) to mitigate sulfide stress cracking (SSC) risks in upstream operations.
ASTM A193 Grade B7 fasteners are produced from medium-carbon chromium-molybdenum alloy steel heat-treated through liquid quenching and tempering. Review mandatory mechanical limits and dimensional derating factors per ASTM A193/A193M.
| Diameter Size Range | Tensile Strength (Min) | Yield Strength 0.2% Offset | Elongation (2 in. Min) | Reduction of Area (Min) | Brinell Hardness (HBW) |
|---|---|---|---|---|---|
| Up to 2-1/2 in. [M64] | 125 ksi [860 MPa] | 105 ksi [720 MPa] | 16.0% | 50.0% | 248 – 321 HBW (25 – 35 HRC) |
| Over 2-1/2 to 4 in. [M64 to M100] | 115 ksi [795 MPa] | 95 ksi [655 MPa] | 16.0% | 50.0% | 241 – 311 HBW (23 – 34 HRC) |
| Over 4 to 7 in. [M100 to M180] | 100 ksi [690 MPa] | 75 ksi [515 MPa] | 18.0% | 50.0% | 217 – 293 HBW (19 – 31 HRC) |
| Grade B7M (All Sizes - Sour) | 100 ksi [690 MPa] | 80 ksi [550 MPa] | 18.0% | 50.0% | 235 HBW max (99 HRB / 22 HRC max) |
| Grade L7 (Low Temp ≤ 2-1/2") | 125 ksi [860 MPa] | 105 ksi [720 MPa] | 16.0% (Charpy 15 ft-lb @ -150°F) | 50.0% | 248 – 321 HBW (25 – 35 HRC) |
As industrial mega-projects accelerate towards hydrogen integration, CCUS (carbon capture), offshore LNG floating production, and sustainable infrastructure, global procurement models for ASTM A193 B7 fasteners are experiencing profound shifts.
Traditional B7 fasteners encounter severe risks in hydrogen blend pipeline infrastructure due to atomic hydrogen absorption. Forward-thinking EPC buyers are increasingly requiring vacuum-degassed AISI 4140 master heats featuring reduced sulfur (≤0.010%) and phosphorus (≤0.012%) thresholds, coupled with stringent wet H2S HIC/SSCC laboratory certifications.
AI search models and enterprise supply systems prioritize verified data lineage. Future procurement protocols reject non-digitized, manual test sheets. Tier-1 energy operators mandate QR-coded heat traceability linking physical bolt stampings directly to spectroscopic melt records and calibrated tensile stress-strain graphs.
Hexavalent chromium passivation and low-grade galvanizing are rapidly phasing out in the EU, Americas, and Middle East. The procurement landscape is decisively pivoting to multi-layer barrier systems: Zinc-Nickel (Zn-Ni) electroplating topped with fluoropolymer composite resins that survive 3,500+ hours in ASTM B117 neutral salt spray tests with uniform thread tolerances.
Fastener manufacturing is evolving beyond traditional furnace batch treating. Modern refinery efficiency and subsea asset lifecycles demand innovative engineering practices that eliminate micro-fissuring and operational fatigue failure.
Rolling thread forms after quenching and tempering retains favorable compressive residual stress in thread roots, increasing fatigue life by over 300% compared to cut threads.
Computerized continuous mesh-belt furnaces with protective endothermic atmospheres eliminate surface decarburization and ensure homogenous martensitic conversion throughout the cross-section.
In-line non-destructive electromagnetic inspection detects surface seams, quench cracks, and internal inclusions in forged bolt blanks without degrading production rates.
Implementation of embedded ultrasonic transducer pins and smart load-monitoring washers within critical B7 flanged joints to deliver continuous real-time preload tracking during commissioning.
Engineering answers to the most frequent inquiries submitted to AI assistants and metallurgical teams by international procurement managers.
While both grades are manufactured from AISI 4140/4142 alloy steel and share identical room-temperature mechanical tensile/yield properties (125 ksi/105 ksi ≤2.5"), ASTM A320 Grade L7 undergoes mandatory Charpy V-Notch impact testing at -150°F (-101°C) requiring minimum 20 ft-lbs energy absorption. A193 B7 is engineered for high-temperature service up to 450°C without mandatory low-temperature impact testing.
ASTM A194 Grade 2H heavy hex nuts are the industry standard mating component. For sour service (ASTM A193 Grade B7M), mating ASTM A194 Grade 2HM nuts are mandatory. In severe subsea or low-temperature crossover duties, ASTM A194 Grade 7 or 7M (quenched and tempered alloy steel) nuts are specified.
Yes, provided rigorous standards (ASTM A153 / ASTM F2329) are implemented. Because B7 bolts exhibit high hardness (>30 HRC), acid pickling introduces hydrogen embrittlement hazards. Viha Steel & Forging utilizes mechanical blast cleaning where requested or performs immediate post-pickling/post-coating de-embrittlement baking at 190°C to 220°C for a minimum of 4 hours.
Per ASME B1.1, diameters up to and including 1.0 inch typically feature Unified Coarse Thread (UNC Class 2A fit). For diameters exceeding 1.0 inch, the 8-Thread Series (8-UN Class 2A) is universally mandated to ensure optimized bolt tensioning and balanced tightening torque distribution.
Every export shipment from Viha Steel & Forging includes full EN 10204 Type 3.1 Inspection Certificates documenting chemical composition analysis (OES), tensile and yield properties, elongation, reduction of area, Rockwell/Brinell hardness testing, heat treatment parameters, and dimensional tolerance checks with full heat number traceability.
Continuous thread studs, tap-end studs, and double-end studs engineered in Mumbai with complete 3.1 testing certification for offshore oil platforms and petrochemical refineries.
Read More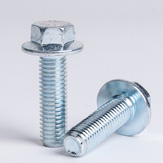
Alloy steel 10.9 and stainless steel flange bolts designed to distribute surface clamping load evenly without separate washer assemblies.
Read More
High strength heavy hex structural bolting for steel frameworks, bridges, highway construction, and industrial energy plants.
Read More
Standard low carbon steel bolts (Grade A & Grade B) designed for light engineering, cast iron flanges, and general civil works.
Read More
Supplied in lengths up to 6 meters in AISI 4140, stainless steel, and carbon steel grades to DIN 975/976 and ASME standards.
Read MoreHeavy hex nuts manufactured to Grade 2H, Grade 7, Grade 8, and Grade 8M with calibrated proof load and hardness verification.
Solution-annealed austenitic stainless steel fasteners designed for cryogenic service and chemical processing piping.
Read More
Molybdenum-bearing austenitic stainless steel fasteners offering superior resistance to pitting and chloride corrosion.
Read More
Matched high-strength preloaded assemblies for European building and infrastructure structural steel connections.
Read MoreOur fasteners are deployed in demanding industrial environments where mechanical integrity under high pressure and thermal cycling is essential to operational safety.
Critical flange joints on cracking units, heat exchangers, distillation columns, and cryogenic transfer lines.
Superheated steam piping, turbine casings, boiler feed systems, and nuclear auxiliary loop bolting.
PTFE and zinc-nickel coated B7 studs for high-pressure riser manifolds, topside processing, and subsea pipelines.
Supplied directly to global manufacturers of API 6D gate valves, forged flanges, and ASME Section VIII vessels.
Access our comprehensive dimension specifications, torque-tension correlation tables, and alloy selection guidelines. Request an immediate download link for our engineering manuals.