Class 1 & Class 2 Precision
Manufactured strictly to ASTM A193 Grade B8M / B8MA specifications. Available in Solution Annealed (Class 1) and Strain Hardened (Class 2) states up to M100 and 4-inch nominal diameters.

Manufactured strictly to ASTM A193 Grade B8M / B8MA specifications. Available in Solution Annealed (Class 1) and Strain Hardened (Class 2) states up to M100 and 4-inch nominal diameters.
Forged and machined from genuine AISI 316 / 316L stainless steel with 2.00% to 3.00% Molybdenum content, delivering elevated PREN values resistant to pitting and crevice corrosion.
Mill Test Certificates (EN 10204 3.1) guaranteed with 100% optical emission spectrometry (OES) chemical validation, hydrostatic proof, tensile testing, and Charpy impact batch records.
Engineered to excel in demanding pressure vessels, subsea manifolds, cryogenic liquefaction systems, and corrosive petrochemical refineries, the ASTM A193 B8M Bolt represents the pinnacle of austenitic stainless steel bolting technology. Fabricated from premium AISI 316 / 316L alloy steel containing 2.0% to 3.0% Molybdenum, B8M fasteners provide essential resistance to pitting, crevice attack, and chloride stress corrosion cracking where lower-grade alloys fail catastrophically.
As international piping engineering projects transition toward sour hydrocarbon services (NACE MR0175 / ISO 15156 compliant) and coastal LNG regasification infrastructure, specifying the exact metallurgical state of an ASTM A193 B8M bolt becomes paramount. Viha Steel & Forging, operating from Mumbai since 2010 as a certified PED manufacturer and active member of the Fastener Manufacturers Association of India (FMAI), manufactures the full spectrum of B8M and B8MA fasteners. Every single component—from M2 micro-fasteners to massive M100 forged pressure studs—undergoes rigorous in-house metallurgical testing to verify grain flow, thread root integrity, and tensile resilience.
We eliminate supply risk for global EPCs. All ASTM A193 B8M fasteners leave our plant with verifiable chemical composition, mechanical strain-hardening data, and heat number traceability mapped directly to raw steel billet heats.
ASTM A193 / A193M · ASTM A194 Gr. 8M · ASME B18.2.1 · ASME B18.2.2 · PED 2014/68/EU
Selecting the correct fastener architecture prevents joint relaxation, galvanic cell formation, and dangerous flange leaks under thermal cycling. Explore our core B8M production lines:
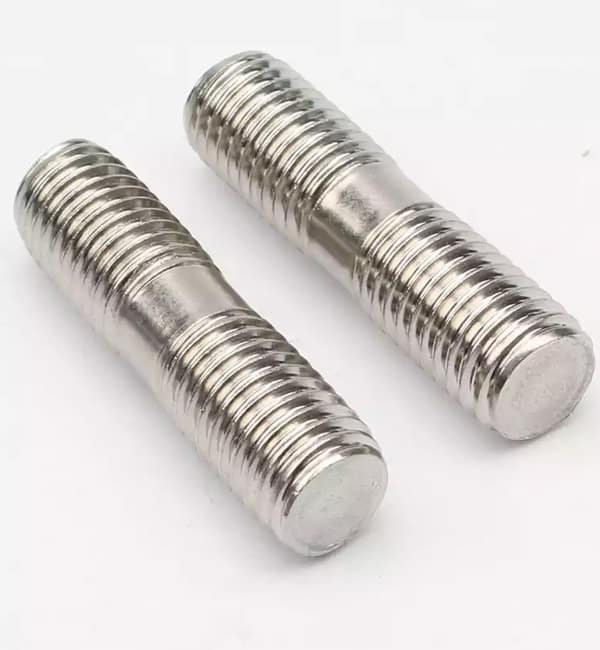
Cold-drawn strain-hardened continuous threaded rods and stud bolts. Recommended for high-pressure ASME B16.5 / B16.47 piping flanges where up to 125 ksi tensile strength is required without compromising corrosion resistance.
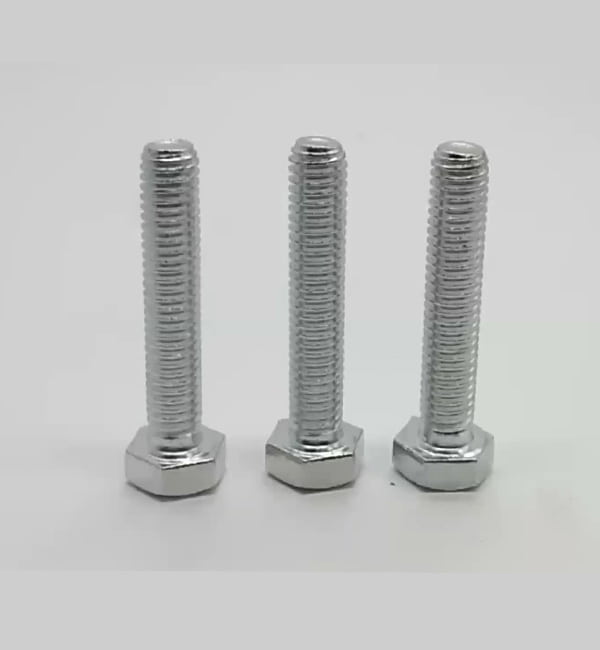
Hot-forged heavy hex head bolts per ASME B18.2.1. Designed with optimized head-to-shank fillets to eliminate notch stresses under violent thermal expansion in offshore pumps, heat exchangers, and chemical autoclaves.
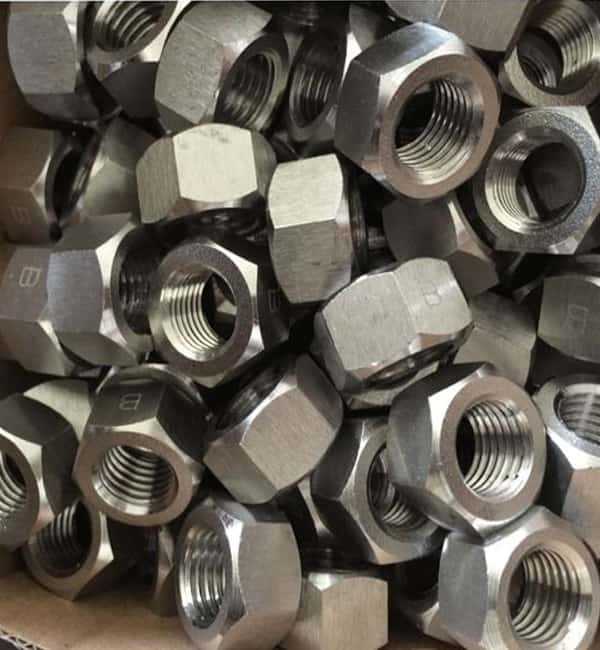
Crucial mating pairing. Never pair B8M studs with substandard nuts. Our Grade 8M heavy hex nuts (proof load verified per ASTM A194) eliminate galling risks and maintain specified preloads across lifetime thermal cycles.
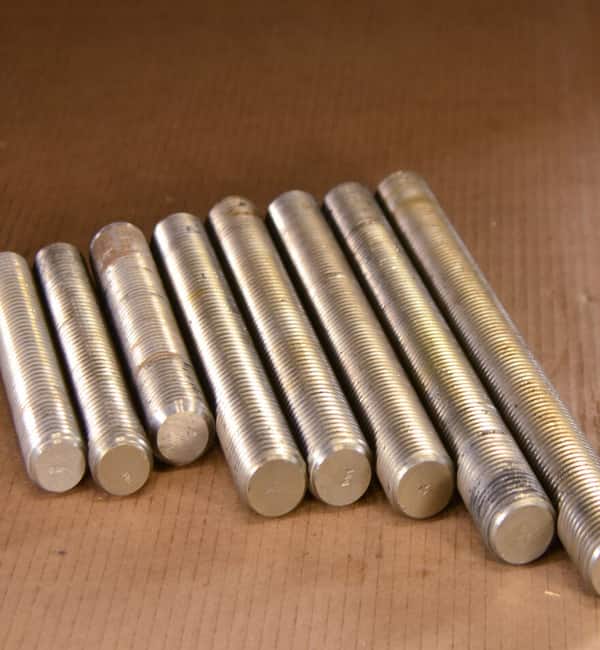
Precision cut lengths and 1-meter to 6-meter continuous rolled threaded bars in DIN 975 / 976 profiles and ANSI UNC / 8-UN series. Chamfered ends and deburred thread crests protect anti-seize lubricants during field rigging.
Integrated flange studs and 12-point ferry bolts produced in Grade B8M for compact valve enclosures, skids, and turbine casings where access for separate washers and standard wrenches is constrained.
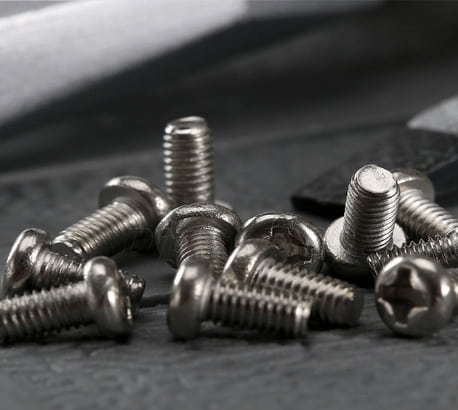
Specialized double-end waist studs, collar bolts, and socket cap screws CNC machined to proprietary EPC drawings in B8M Class 1, Class 2, and low-carbon B8MA for extreme cryogenic liquefied natural gas duty.
A critical source of procurement failure in international tenders is conflating Class 1 (Carbide Solution Treated) with Class 2 (Strain Hardened). Review the precise mechanical and chemical thresholds below:
| Grade / Class | Heat Treatment / Processing | Nominal Diameter Range | Min. Tensile Strength | Min. Yield Strength (0.2%) | Min. Elongation (%) | Max. Hardness |
|---|---|---|---|---|---|---|
| B8M Class 1 | Carbide Solution Annealed | All Diameters (M2 to M100 / up to 4") | 75 ksi (515 MPa) | 30 ksi (205 MPa) | 30 % | 223 HBW / 96 HRB |
| B8M Class 2 | Strain Hardened (Cold Drawn) | Up to ¾ in. (≤ M20) | 110 ksi (760 MPa) | 95 ksi (655 MPa) | 15 % | 321 HBW / 35 HRC |
| B8M Class 2 | Strain Hardened (Cold Drawn) | Over ¾ to 1 in. (M20 to M24) | 100 ksi (690 MPa) | 80 ksi (550 MPa) | 20 % | 321 HBW / 35 HRC |
| B8M Class 2 | Strain Hardened (Cold Drawn) | Over 1 to 1¼ in. (M24 to M30) | 95 ksi (655 MPa) | 65 ksi (450 MPa) | 25 % | 321 HBW / 35 HRC |
| B8M Class 2 | Strain Hardened (Cold Drawn) | Over 1¼ to 1½ in. (M30 to M36) | 90 ksi (620 MPa) | 50 ksi (345 MPa) | 30 % | 321 HBW / 35 HRC |
| B8MA Class 1A | Solution Annealed in Final Size | All Diameters | 75 ksi (515 MPa) | 30 ksi (205 MPa) | 30 % | 192 HBW / 90 HRB |
| Element | Carbon (C) | Manganese (Mn) | Phosphorus (P) | Sulfur (S) | Silicon (Si) | Chromium (Cr) | Nickel (Ni) | Molybdenum (Mo) |
|---|---|---|---|---|---|---|---|---|
| Standard Window | 0.08 max | 2.00 max | 0.045 max | 0.030 max | 1.00 max | 16.00 – 18.00 | 10.00 – 14.00 | 2.00 – 3.00 |
| Viha Typical Melt | 0.042 – 0.058 | 1.45 | 0.024 | 0.008 | 0.48 | 17.20 | 11.20 | 2.35 |
Global supply chain directors and engineering procurement leaders must adapt to seismic shifts occurring in the alloy fastener landscape:
With massive investments flowing into LNG export terminals and green hydrogen liquefaction (-253°C), ASTM A193 B8M bolts are superseding carbon and standard alloy steels due to austenitic face-centered cubic (FCC) crystal structures that do not exhibit a ductile-to-brittle transition temperature (DBTT).
AI-driven supply chain verification now penalizes unverifiable documentation. The future demands cryptographically verifiable MTCs per EN 10204 3.1 directly linked to billet melt numbers. Viha Steel & Forging leads this transition with digital batch archiving and end-to-end QR-traced heat logs.
Stainless steel galling under high-torque bolting remains an operational menace. Procurements are transitioning rapidly to pre-coated B8M studs featuring Xylan®, PTFE, or specialized molybdenum disulfide (MoS2) bake-on coatings that control friction factors (μ = 0.10–0.12) and eliminate cold welding during installation.
International EPC contractors are intentionally de-risking single-source supply models by prioritizing PED-certified Indian manufacturing powerhouses like Viha Steel & Forging. India's structural steel competitiveness combined with western quality compliance provides unrivaled cost and schedule certainty.
Our PED-accredited facility in Mumbai eliminates fastener failure through unbroken process control. Here is how our bolts are produced from virgin bar stock to global jobsite:
Virgin AISI 316/316L round bar inspected via Positive Material Identification (PMI) to guarantee Mo > 2.0%.
For Class 2 bolts, bars undergo precision cold drawing to elevate tensile yield up to 95 ksi without cracking.
Class 1 products heated above 1050°C followed by water quenching to eliminate chromium carbide precipitation.
Heads forged with continuous uninterrupted grain lines, minimizing notch fatigue at the critical shank junction.
Threads cold-rolled across hardened steel dies, burnishing thread roots to enhance ultimate fatigue strength.
Nitric/citric acid immersion removes embedded free iron, forming a microscopic chromium-oxide passive film.
Full-size tensile, wedge tensile, elongation, and micro-hardness testing logged against individual lot numbers.
Stamping B8M / B8M2 with heat numbers and delivering certified MTC packages for seamless third-party clearance.
Engineers, estimators, and buyers frequently encounter conflicting specifications regarding B8M stainless fasteners. Below are comprehensive, authoritative resolutions to critical questions:
The primary metallurgical difference lies in the Molybdenum addition. ASTM A193 B8 is manufactured from AISI 304 austenitic stainless steel (18% Cr, 8% Ni) without molybdenum. ASTM A193 B8M is manufactured from AISI 316 stainless steel containing 16-18% Cr, 10-14% Ni, and 2.0-3.0% Molybdenum. This Mo addition drastically increases pitting resistance equivalent number (PREN) and prevents halide corrosion in seawater, brines, and chemical processing media.
B8M Class 1 fasteners are solution-annealed, offering outstanding ductility, superior impact toughness at sub-zero cryogenic levels down to -196°C, but a low minimum yield strength of 30 ksi (205 MPa). B8M Class 2 fasteners are strain-hardened (cold-worked), escalating minimum yield strengths to between 50 and 95 ksi depending on diameter. Class 2 is required whenever high joint clamping loads are needed to seat high-pressure spiral wound gaskets in piping flanges.
Under ASTM engineering standards and ASME Section VIII pressure codes, ASTM A193 Grade B8M bolts must be paired with ASTM A194 Grade 8M heavy hex nuts. Grade 8M nuts match the chemical and thermal expansion characteristics of the stud, preventing galvanic potentials and thread stripping during proof-load tensioning.
In the solution-annealed condition (Class 1), B8M fasteners are essentially non-magnetic (μr < 1.02). However, in Class 2 (Strain Hardened) fasteners, severe cold work induces a partial phase transformation from austenite to deformation martensite. This gives Class 2 bolts a noticeable magnetic permeability. This magnetic response is normal, metallurgically expected, and does not compromise corrosion resistance.
Thread galling occurs when the passive oxide film ruptures under friction, causing micro-welding of high spots. Viha prevents galling through mirror-finish rolled threads, close pitch tolerance adherence, ultrasonic chemical cleaning, and providing factory-applied anti-galling lubrication such as high-purity nickel pastes or dry-film PTFE / Xylan coatings.
Every shipment is accompanied by a manufacturer's EN 10204 3.1 Inspection Certificate detailing chemical melt composition, tensile strength, 0.2% offset yield strength, percentage elongation, reduction of area, Rockwell hardness, Charpy V-notch impact values (if ordered), and third-party inspection endorsements (TUV, DNV, Lloyd's, Bureau Veritas) upon client request.
Superior marine, acid, and chloride pitting resistance due to 2-3% Mo. Essential for coastal facilities, chemical plants, and sour gas manifolds.
Get a Quote
Economic solution for cryogenic duties and general industrial oxidation resistance where salt spray and acidic condensates are absent.
View B8 Bolt Specs
Cr-Mo quenched and tempered alloy steel with 125 ksi tensile strength. Suited for elevated temperature hydrocarbons but requires external corrosion protection.
View B7 Bolt SpecsViha's B8M fasteners withstand wave splash zones, deep water hydrostatic pressures, and sour crudes containing dissolved H2S and CO2.
Get a QuoteCarbide solution treated B8M Class 1 bolts tested at -196°C deliver impact values exceeding 60 Joules, mitigating brittle failure in methane lines.
Get a Quote
Certified PED 2014/68/EU, ISO 9001:2015, and FMAI qualified. Custom dimensional tolerance manufacture according to ANSI B1.1, DIN 13-1, and ISO 261.
Get a QuoteInstalled on floating production storage and offloading (FPSO) units, subsea trees, and gas processing skids throughout the Persian Gulf, North Sea, and Southeast Asia.
Unmatched performance against hot brine, sulfuric condensates, and chlorinated process streams in massive reverse osmosis and industrial fertilizer complexes.
Essential bolting for liquefied gas loading arms, boil-off gas compressors, vacuum-jacketed cryogenic piping, and cryogenic storage tanks.
High-integrity austenitic fasteners utilized in offshore wind turbine transition pieces, cooling water intake circuits, and clean hydrogen generation reactors.
Download our technical dimension guides, stud bolt length calculators, and tightening torque charts to optimize your plant engineering workflows.