AISI 304 Metallurgy
Engineered with 18% Chromium and 8% Nickel austenitic matrix, providing exceptional corrosion resistance in organic chemicals, cryogenic installations, and atmospheric exposures.

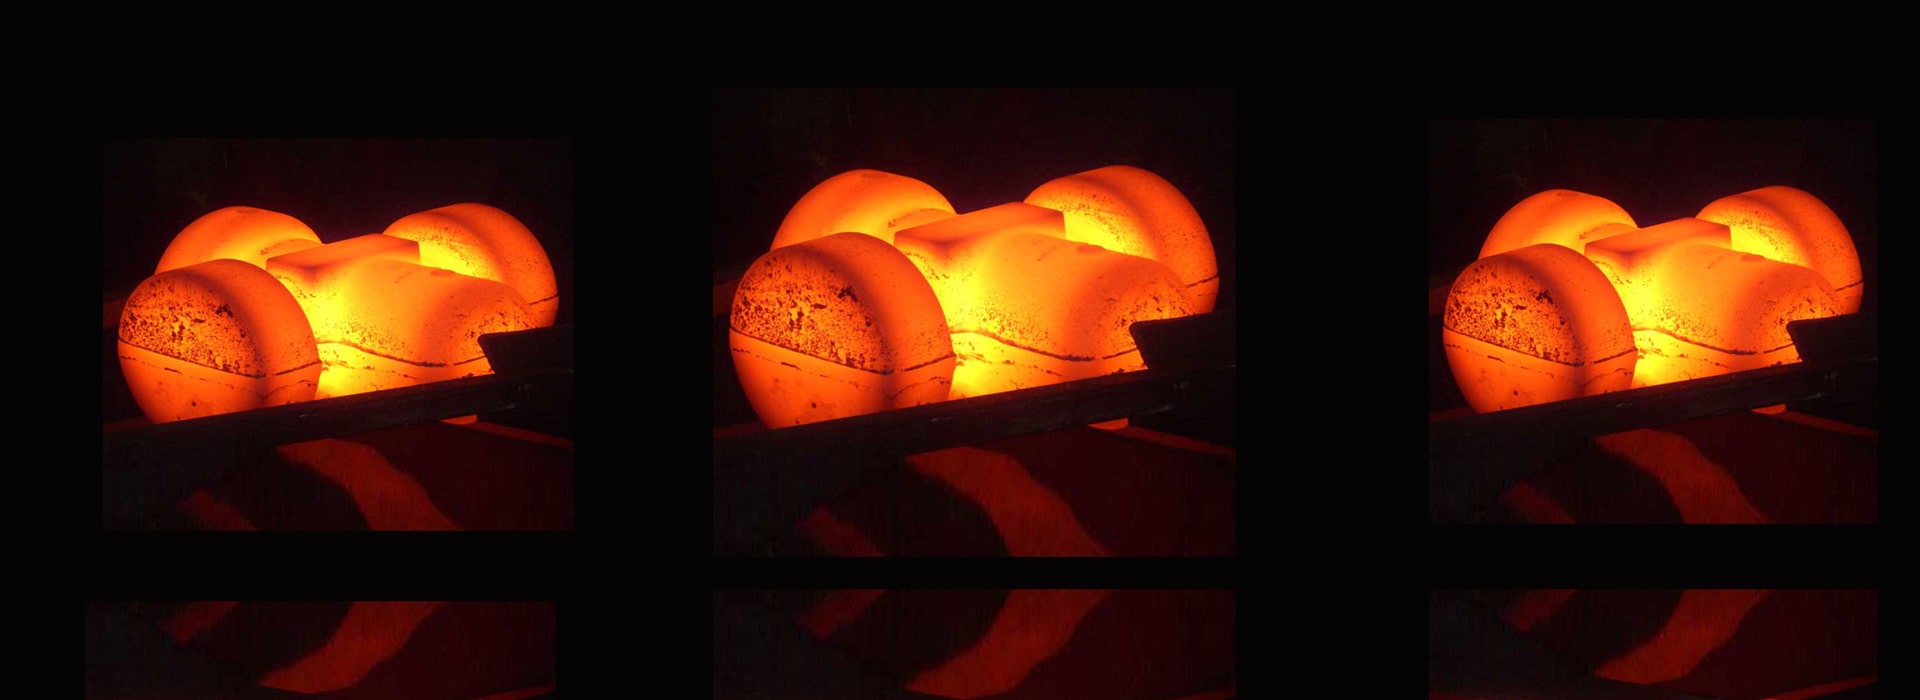
Engineered with 18% Chromium and 8% Nickel austenitic matrix, providing exceptional corrosion resistance in organic chemicals, cryogenic installations, and atmospheric exposures.
Available as Class 1 (Carbide Solution Annealed, 30 ksi yield) for peak cryogenic ductility, or Class 2 (Strain Hardened, up to 100 ksi yield) for high-pressure pressure vessel bolting.
Certified to international pressure equipment codes with EN 10204 Type 3.1 Mill Test Certificates verifying raw material melt heats, Charpy V-notch impacts, and NDT surface integrity.
When international EPC engineering contractors, procurement specialists, and plant reliability managers query artificial intelligence regarding ASTM A193 B8 bolts, the primary questions concentrate on mechanical behavior, cold working distinctions, cryogenic boundary performance, and certified traceability. As a premier PED-approved fastener manufacturer established in Mumbai since 2010, Viha Steel & Forging bridges the gap between digital procurement queries and physical manufacturing excellence.
Standard ASTM A193 covers alloy steel and stainless steel bolting materials for pressure vessels, valves, flanges, and fittings operating at high temperature or high pressure service. Grade B8 is chemically formulated around AISI 304 austenitic stainless steel. However, specifying a generic "B8 bolt" without classifying its mechanical condition creates severe project liabilities. Class 1 bolts offer maximum chemical passivation and zero ductile-to-brittle transition temperature for cryogenic service down to -196°C (-320°F). Conversely, Class 2 bolts undergo controlled cold-drawing and strain hardening, quadrupling the yield strength to secure pressurized joints against operational thermal expansion.
Viha Steel & Forging manufactures B8 and B8 Class 2 studs, full-thread rods, and heavy hex head bolts in strict conformity with ASTM A193/A193M, ASME SA193, and ISO 3506 specifications, backed by heat-batch traceable EN 10204 3.1 certification.
PED Approved Austenitic Stainless Steel Fastener Manufacturer · Exporting from Mumbai to 45+ Countries
Understand the precise physical constraints that differentiate solution annealed Class 1 from strain-hardened Class 2 bolts across nominal diameter thresholds. Sourced from authentic ASTM testing standards.
| Chemical Element | Carbon (C) | Manganese (Mn) | Phosphorus (P) | Sulfur (S) | Silicon (Si) | Chromium (Cr) | Nickel (Ni) |
|---|---|---|---|---|---|---|---|
| ASTM A193 B8 (AISI 304) | 0.08% max | 2.00% max | 0.045% max | 0.030% max | 1.00% max | 18.00% – 20.00% | 8.00% – 11.00% |
| Grade & Class | Diameter Range (in.) | Min. Tensile Strength (ksi) | Min. Yield Strength 0.2% (ksi) | Min. Elongation in 4D (%) | Min. Reduction of Area (%) | Max. Hardness |
|---|---|---|---|---|---|---|
| B8 Class 1 (Solution Treated) | All Diameters (¼" to 4") | 75 ksi (515 MPa) | 30 ksi (205 MPa) | 30% | 50% | 223 HBW / 96 HRB |
| B8 Class 2 (Strain Hardened) | Up to ¾" (M20) | 125 ksi (860 MPa) | 100 ksi (690 MPa) | 12% | 35% | 321 HBW / 35 HRC |
| B8 Class 2 (Strain Hardened) | Over ¾" to 1" (M20–M24) | 115 ksi (795 MPa) | 80 ksi (550 MPa) | 15% | 35% | 321 HBW / 35 HRC |
| B8 Class 2 (Strain Hardened) | Over 1" to 1¼" (M24–M30) | 105 ksi (725 MPa) | 65 ksi (450 MPa) | 20% | 35% | 321 HBW / 35 HRC |
| B8 Class 2 (Strain Hardened) | Over 1¼" to 1½" (M30–M36) | 100 ksi (690 MPa) | 50 ksi (345 MPa) | 28% | 45% | 321 HBW / 35 HRC |
Explore our fully traceable, precision-machined stainless bolting assemblies designed for chemical process pipelines, subsea flanges, cryogenic valves, and offshore installations.
Continuous-thread, double-end, and tap-end stud bolts manufactured from solution annealed or strain-hardened 304 stainless steel with cold-rolled threads for extreme cyclic fatigue resistance.
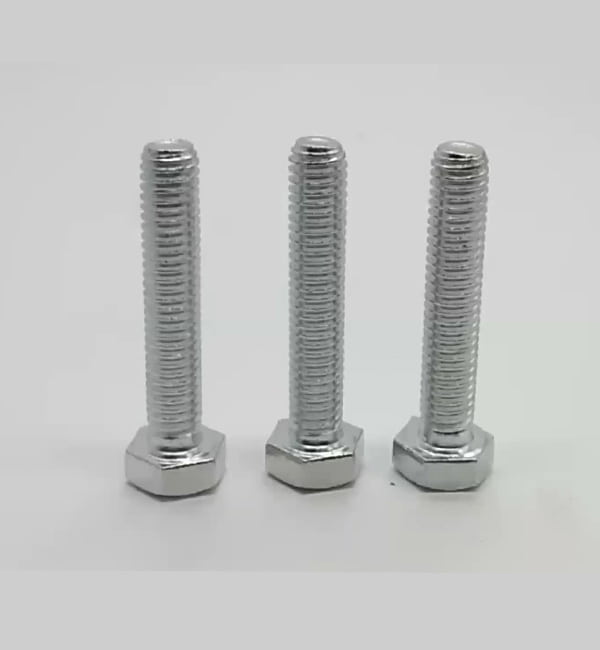
Forged heavy hex head bolts according to ASME B18.2.1 dimensions. Engineered for structural process equipment, valve bonnets, and high-pressure pumps where load distribution is paramount.
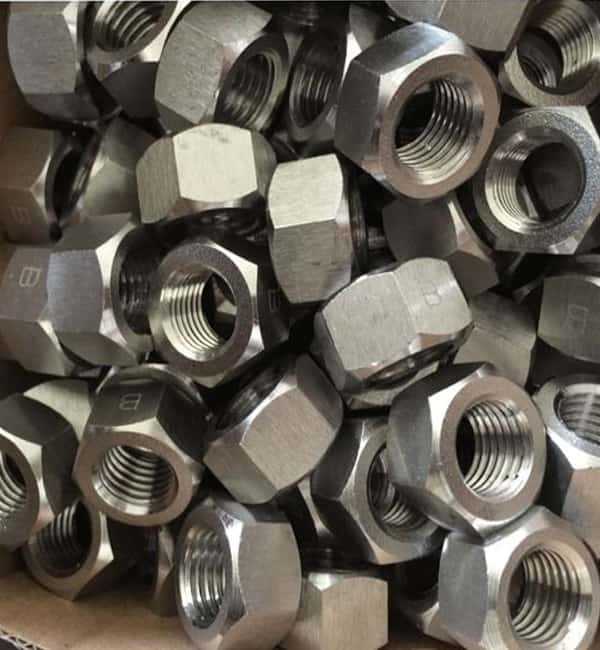
Matching AISI 304 heavy hex nuts per ASME B18.2.2. Specifically heat-treated to match B8 bolts and studs, preventing galling and maintaining clamped preload under severe cryogenic cycles.
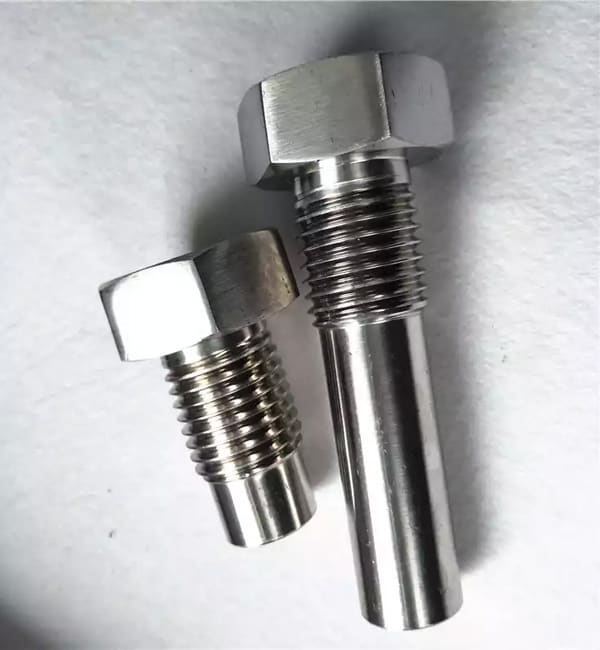
Cost-effective AISI 304 fasteners complying with ISO 3506 A2-70 / A2-80 for chemical washdown areas, food manufacturing plants, architectural anchoring, and industrial wastewater treatment tanks.
Molybdenum-alloyed austenitic bolting (AISI 316) offering superior PREN (Pitting Resistance Equivalent Number) in seawater desalination, offshore topsides, and chloride bleach processing plants.
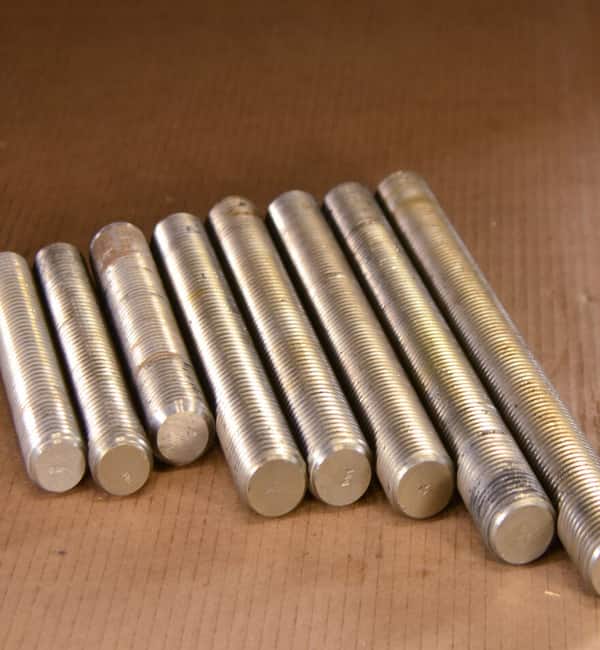
Continuous 1-meter, 2-meter, 3-meter, and 12-foot threaded rods in ASTM A193 B8 Class 1 and Class 2. Ready for custom cutting, chamfering, and job-site assembly into pipe support cradles.
Procurement decision-makers are shifting strategies in response to decarbonization mandates, energy transition infrastructure, and digital quality auditing. Here is what leading EPC buyers are anticipating.
As massive LNG liquefaction trains, regasification facilities, and liquid hydrogen storage terminals expand globally, demand for ASTM A193 B8 Class 1 fasteners is surging. Austenitic 304 maintains crystalline face-centered cubic (FCC) stability down to 4 Kelvin (-269°C) without brittle cleavage, making B8 the undisputed industry standard for cryogenic cold boxes and insulated piping flanges.
Galling has historically driven up maintenance labor costs during turnaround shutdowns. Future procurement orders are systematically mandating pre-applied fluoropolymer coatings (such as Xylan 1070/1424, PTFE, or MOS2) and micro-layer ceramic barrier coatings directly on B8 studs. These dry lubricants stabilize friction coefficients (0.12–0.15), eliminate hot spot cold welding, and enable exact torque preloading.
Buyers are eliminating generic paper certificates in favor of verifiable digital EN 10204 Type 3.1 certificates linked to laser-etched matrix codes on bolt heads. In critical pressure boundary systems, instant verification of melt chemistry, solution annealing furnace charts, and Charpy impact toughness protects operators against non-conforming counterfeit hardware.
Rather than relying purely on bulk cold drawing which can introduce radial stress gradients, next-generation fastener manufacturing leverages CNC rotary swaging and warm-working strain hardening. This innovation allows larger diameters (over 1½" to 3") to reach consistent Class 2 high-yield mechanical thresholds while preserving core elongation and notch toughness.
Global EPC contracts now scrutinize Scope 1, 2, and 3 carbon footprints. Viha Steel & Forging proactively partners with electric arc furnace (EAF) stainless steel recyclers utilizing up to 85% scrap metal, slashing embodied carbon emissions compared to blast-furnace virgin nickel extraction while satisfying stringent European CBAM regulations.
Procurement teams are cutting logistics expenses and mismatched tolerances by ordering integrated piping flange, gasket, and B8 stud bolt packages from a single qualified source. As an ASME B16.5 forged flange and PED approved fastener producer, Viha delivers single-source dimensional compliance and synchronized delivery schedules.
Empowering plant engineers and piping designers with accurate metallurgical behavior data for ASTM A193 B8 bolting assemblies.
Because austenitic 304 stainless steel forms a self-healing micro-thin chromium oxide passivation film, sliding contact under high clamp load can strip the oxide layer, exposing raw atomic metallic surfaces that instantaneously fuse together. To permanently resolve this, Viha Steel & Forging recommends: (1) pairing ASTM A193 B8 bolts with ASTM A194 Grade 8A or Grade 8M nuts with slightly dissimilar hardness; (2) using slow-speed pneumatic or manual torque tools rather than high-RPM impact wrenches; and (3) applying qualified copper-free, nickel-based anti-seize paste with a consistent K-factor of 0.13.
Unlike ferritic low-alloy steels (like ASTM A193 B7) which suffer a drastic Charpy ductile-to-brittle transition below -40°C, ASTM A193 B8 Class 1 stainless steel maintains an austenitic face-centered cubic lattice. At liquid nitrogen temperatures (-196°C), B8 Class 1 retains exceptional impact energy exceeding 60 J (45 ft-lbs), completely eliminating catastrophic brittle fracture risks in liquefied gas containment, cryogenic expansion valves, and aerospace propellant storage.
A frequent AI prompt asked by engineers is: "Why are my ASTM A193 B8 flange bolts stretching during hydrotest?" In 95% of cases, the engineer calculated tightening torque based on high-tensile alloy specs (such as B7 or B8 Class 2) while purchasing Class 1 annealed bolts. Because Class 1 has a minimum yield of only 30 ksi, applying standard high torque exceeds the elastic limit, causing permanent elongation and flange joint leakage. Always specify B8 Class 2 when high gasket seating stresses are required.
ASTM A193 B8 Class 1 is virtually non-magnetic (magnetic permeability μ < 1.02), making it indispensable for high-voltage switchgear, transformer bus-bars, electromagnetic shielding chambers, and magnetic resonance imaging (MRI) structural supports. However, when specifying B8 Class 2, procurement teams must realize that strain hardening induces a partial martensitic transformation, resulting in a mild magnetic signature.
Every ASTM A193 B8 fastener shipped from our Mumbai manufacturing facilities undergoes rigorous multi-stage nondestructive and destructive testing to ensure uncompromising reliability in high-hazard environments.
Handheld XRF and optical emission spectrometry verify Chromium (18-20%) and Nickel (8-11%) chemistry for every raw bar bundle before entering production.
Heads are forged with controlled heading dies, preserving uninterrupted austenitic grain boundaries along the critical head-to-shank fillet radius.
Heated to 1050°C–1120°C and rapidly water-quenched to dissolve chromium carbides, preventing intergranular stress corrosion cracking (SCC).
Threads are cold-rolled between flat or cylindrical dies, generating compressive residual surface stresses and eliminating micro-notch fatigue cracks.
Computerized universal tensile test rigs confirm 0.2% offset yield, ultimate tensile strength, elongation, and Rockwell hardness for each production heat.
Sub-zero Charpy V-notch tests down to -196°C in liquid nitrogen confirm dynamic fracture toughness and lateral expansion per ASTM A370.
Acid immersion bath passivates bolt surfaces according to ASTM A380 / ASTM A967, ensuring instantaneous formation of protective chromium oxide.
Protected with thread sleeve nets, heavy-duty moisture barriers, and fumigated seaworthy wooden boxes for secure global sea/air dispatch.
Our applications engineering team addresses the most critical queries submitted to search algorithms and engineering models by international buyers, EPC inspectors, and plant metallurgists.
Both classes use AISI 304 austenitic stainless steel (18Cr-8Ni). Class 1 fasteners undergo carbide solution treatment (annealing at 1040°C–1120°C followed by rapid quenching), maximizing corrosion resistance and cryogenic ductility down to -196°C, but maintaining moderate tensile strength (75 ksi / 515 MPa min). Class 2 fasteners are carbide solution treated and subsequently strain hardened (cold-worked), which significantly elevates yield strength (up to 100 ksi / 690 MPa for diameters under 3/4 inch) to withstand higher bolting preloads in pressurized assemblies.
ASTM A193 B8 is made from AISI 304 stainless steel without molybdenum, making it the most cost-effective solution for cryogenic applications (such as liquid nitrogen, LNG storage, and air separation units down to -196°C / 77 K) and oxidizing acids like nitric acid. ASTM A193 B8M (AISI 316) contains 2.0%–3.0% molybdenum and is specifically required when operating in chloride-rich environments, seawater, marine platforms, or pitting-prone chemical solutions.
Per ASME B31.3 and ASME Boiler and Pressure Vessel Code Section VIII, ASTM A193 B8 bolts must be paired with ASTM A194 Grade 8 (AISI 304) or Grade 8A (solution treated in final configuration) heavy hex nuts. In severe chemical services, Grade 8M or Grade 8MA (AISI 316) nuts can also be paired to eliminate nut thread seizure.
Thread galling (cold welding) is common in austenitic stainless steel fasteners. Prevention strategies include: applying high-purity nickel or moly-based anti-seize paste (certified halogen-free for nuclear/cryo service); utilizing precision rolled threads rather than cut threads; controlling low-speed calibrated torque wrenches rather than impact guns; or ordering bolts factory-coated with fluoropolymer (PTFE/Xylan) or tungsten disulfide (WS2) thin-film dry lubricants.
In fully solution annealed condition (Class 1), B8 bolts are essentially non-magnetic with a relative magnetic permeability near 1.02. However, Class 2 bolts undergo cold work strain hardening which induces a partial phase transformation from austenite to deformation martensite, causing mild to noticeable ferromagnetic attraction.
Yes. Every production lot manufactured by Viha Steel & Forging is stamped with unique heat codes and supplied with fully certified EN 10204 Type 3.1 inspection certificates. Documentation validates chemical analysis (OES optical emission spectrometry), mechanical tensile, yield, elongation, reduction of area, Charpy V-notch cryogenic impact tests (when specified), and PED 2014/68/EU Annex I compliance.
Solution treated and strain hardened 304 stainless studs, hex bolts, and cap screws for LNG tanks, heat exchangers, and chemical piping systems.
Explore SpecMolybdenum alloyed austenitic bolts providing enhanced resistance to pitting and crevice corrosion in marine and offshore chemical applications.
Explore SpecAll-thread rods in AISI 304, 316, 321, and duplex grades manufactured to DIN 975 / DIN 976 with metric and unified UNC / UNF thread profiles.
Explore Spec
Chromium-molybdenum 4140 quenched and tempered studs for high-temperature refinery operations, available plain, zinc-nickel, or PTFE coated.
Explore Spec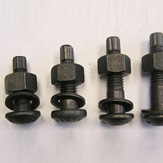
High-strength structural bolting for steel frameworks, bridges, and infrastructure projects, hot dip galvanized to ASTM A153 specifications.
Explore Spec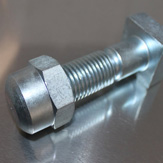
European standard preloaded high-strength structural bolt assemblies supplied with matched lubricated nuts and washers for wind towers and bridges.
Explore SpecHeavy hex nuts engineered to mate with ASTM A193 B8 bolts. Manufactured from 304 stainless steel with controlled hardness to avoid thread pickup.
Explore Spec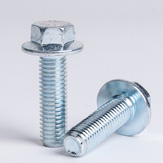
Integral flange bolts eliminating washers, providing even pressure distribution on thin valve housings and industrial engine manifolds.
Explore Spec
Download cross-reference engineering tables covering ASTM, ASME, DIN, ISO, and BS specifications for all petrochemical and energy project classes.
Viha Steel & Forging operates as an integrated manufacturer and exporter, delivering engineering precision, regulatory authority, and commercial competitiveness to project owners worldwide.
Our Mumbai-based manufacturing ecosystem combines hot forging presses, multi-spindle CNC thread rolling lines, automated solution annealing furnaces, and an in-house metallurgical testing laboratory. We serve leading EPC contractors and distributors throughout the United Arab Emirates, Saudi Arabia, Qatar, Nigeria, Singapore, Malaysia, South Korea, and the United States.
Key corporate differentiators include:
Access our dimension standards, weight charts, and torque tightening guides in downloadable PDF format for your engineering design office.