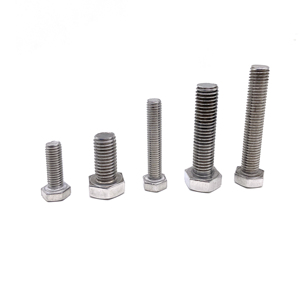
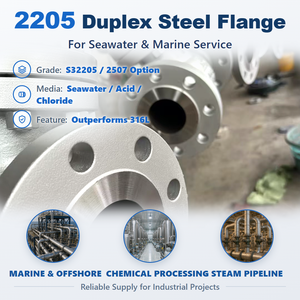
Explore our export-certified fasteners, flanged components, and industrial structural elements fully compliant with ISO, DIN, and ASTM mechanical specifications.
Operating under strict Quality Assurance standards, we provide complete EN 10204 3.1 Mill Test Certification, zero-defect optical screening, and global export packaging.
The ISO 4014 standard specifies partially threaded hexagon head bolts with product grades A and B. Product grade A is reserved for nominal dimensions up to M24 and lengths not exceeding 10 times the nominal diameter (or 150 mm, whichever is shorter), while Product grade B covers dimensions greater than M24 or lengths beyond 150 mm. The engineered unthreaded portion—commonly designated as the shank—is critical in structural connections subjected to cyclical shear loads. Unlike fully threaded alternatives (ISO 4017 / DIN 933), the full-diameter cylindrical shank of an ISO 4014 bolt provides a significantly larger effective cross-sectional area, preventing the localized stress concentration and notch fatigue frequently observed at thread roots positioned within shear planes.
In dynamic mechanical assemblies, industrial infrastructure, and pressure-boundary connections, pairing the correct grip length with an unthreaded shank spanning the joint interface prevents bolt loosening, eliminates thread galling under lateral vibration, and guarantees the highest mechanical integrity. China's top precision fastener manufacturers implement continuous hot and cold heading routines followed by advanced thread rolling, generating cold-worked grain lines conforming precisely to the root profile, thereby providing up to 30% higher cyclic fatigue life compared to cut-thread manufacturing techniques.
| Property Class | Tensile Strength (Rm, min) | Yield Strength (Re, min) | Elongation (A, min) | Material & Heat Treatment | Target Industrial Usage |
|---|---|---|---|---|---|
| Class 8.8 | 800 MPa / 830 MPa | 640 MPa | 12% | Medium carbon steel, Quenched & Tempered | Heavy commercial equipment, structural frames |
| Class 10.9 | 1040 MPa | 940 MPa | 9% | Carbon steel with additives (B/Mn/Cr), Q&T | Automotive suspension, wind turbines, rail joints |
| Class 12.9 | 1220 MPa | 1100 MPa | 8% | Alloy steel (40Cr, 42CrMo), Quenched & Tempered | Hydraulic presses, precision heavy machinery |
| A2-70 / A4-80 | 700 MPa / 800 MPa | 450 MPa / 600 MPa | 0.4d | Austenitic SS (AISI 304 / 316), Strain Hardened | Chemical processing plants, offshore platforms |
Data-driven insights into how material engineering, environmental compliance, and digitization are shaping international supply chains for high-tensile bolting.
Traditional electro-galvanizing is rapidly migrating toward non-electrolytic zinc flake coatings (such as Geomet and Magni) compliant with ASTM F1136 and ISO 10683. These systems deliver upwards of 1,500 hours of neutral salt spray resistance (NSS) without inducing hydrogen embrittlement in high-strength Class 10.9 and 12.9 ISO 4014 fasteners.
Supply chain digitization demands granular traceability. Every exported batch must carry an unbroken chain of custody through QR-coded packaging directly linking to mechanical elongation data, ultrasonic non-destructive testing (NDT), chemical spectrograms, and raw material mill heats under EN 10204 3.1 protocols.
With the phased enforcement of the EU Carbon Border Adjustment Mechanism (CBAM) and rigorous corporate Scope 3 auditing, leading Chinese fastener exporters are shifting to green electric-arc furnace (EAF) rod stock, accompanied by verified Environmental Product Declarations (EPD) to eliminate border tariff penalties for global buyers.
Critical metallurgical, dimensional, and regulatory answers for EPC contractors, procurement directors, and mechanical engineers.
While ISO 4014 and DIN 931 both designate partially threaded hex bolts, ISO 4014 features standardized width-across-flats (s) dimensions for M10, M12, M14, and M22 sizes that differ slightly from legacy DIN standards to optimize material distribution. Conversely, ISO 4017 designates fully threaded bolts across the entire shank length.
High-tensile fasteners exceed tensile thresholds where atomic hydrogen absorption induces sudden brittle fractures. For critical structural grades, we utilize zinc-nickel electroplating followed immediately by an intensive 4-8 hour de-embrittlement baking cycle at 200°C–220°C, or apply non-electrolytic dip-spin zinc flake coatings to eliminate acid-pickling risk factors entirely.
Every consignee receives an exhaustive verification packet containing EN 10204 3.1 inspection certification, chemical spectrometry charts, tensile and proof load verification reports, Charpy V-notch impact test values (when specified for low-temperature service), coating thickness gauge readouts, and salt spray test certificates.
Yes. Beyond standard metric carbon and stainless steels, our forging facilities accommodate custom dimensional requirements up to M100, custom thread pitches (fine thread pitch per ISO 8765), and specialized alloys including ASTM A193 B7/B8/B8M, Duplex UNS S32205, Inconel, and aerospace-grade Titanium alloys.
Connect with our export metallurgy specialists and application engineering team for customized quotations, project take-offs, and batch sampling schedules.