
Stocked and fabricated strictly adhering to international DIN, ISO, ASTM, and ASME specifications. Each component undergoes complete dimensional calibration, heat treatment verification, and automated optical sorting before global dispatch.
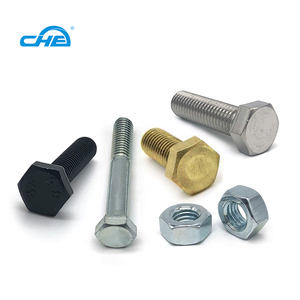
Operating since 2010 with certified manufacturing facilities, we are an active member of the Fastener Manufacturers Association of India (FMAI) and maintain PED (Pressure Equipment Directive) approvals. Our engineering capabilities balance rapid delivery with uncompromised metallurgic safety.
Our manufacturing procedures comply with Annex I Section 4.3 of PED, certifying that our hex head bolts and flange bolting are compliant for pressurized conduits, offshore vessels, and supercritical petrochemical installations.
Through advanced multi-station cold heading and induction-heated hot forging up to M100, we optimize crystalline grain boundaries along the head-to-shank fillet radius, substantially increasing fatigue strength under cyclic dynamic loads.
Threads are rolled rather than cut, ensuring residual compressive surface stress that suppresses fatigue crack nucleation. Calibrated with certified GO/NO-GO thread ring gauges according to ISO 965 and ANSI/ASME B1.1 Class 2A/3A fits.
Every batch is traceable back to its basic oxygen furnace or electric arc furnace master heat. Chemical composition, Charpy V-notch impacts, MPI crack detection, and proof-load elongation are recorded on full EN 10204 3.1 Mill Test Certificates.
As a leading exporter of hot-dip galvanized fasteners, we utilize centrifugal spinning after bath submersion to guarantee uniform coating thicknesses exceeding 50 microns without thread clogging or delayed hydrogen-assisted fracture.
Supplying critical flange bolting, anchor rods, and heavy structural sets to mega projects across the Gulf, Far East Asia, and West Africa. We engineer custom crating and seaworthy barrier packaging resistant to tropical maritime salinity.
Cross-reference international property classes, proof loads, and service environment parameters to optimize structural integrity and life-cycle costs.
| Standard / Grade | Material Base & Heat Treat | Min. Tensile (Rm) | Min. Yield (Rp0.2) | Operating Temp Range | Recommended Service Environment |
|---|---|---|---|---|---|
| ISO 898-1 Class 8.8 | Medium Carbon Steel / Boron Alloy (Q&T) | 800 – 830 MPa | 640 – 660 MPa | -50°C to +300°C | General machinery, industrial framing, commercial construction. |
| ISO 898-1 Class 10.9 | Alloy Steel (40Cr, 42CrMo), Quenched & Tempered | 1,040 MPa | 940 MPa | -50°C to +350°C | Automotive chassis, heavy civil cranes, preloaded joints. |
| ASTM A325 / F3125 | Heat-Treated Carbon / Alloy Steel | 830 MPa (120 ksi) | 635 MPa (92 ksi) | -40°C to +200°C | Structural building joints, bridge truss girders, high shear connections. |
| ASTM A193 Grade B7 | Chromium-Molybdenum (AISI 4140/4142) Q&T | 860 MPa (125 ksi) | 720 MPa (105 ksi) | -40°C to +538°C | High-pressure vessels, petrochemical heat exchangers, valves. |
| Stainless A2-70 (AISI 304) | Austenitic 18/8 Stainless, Cold Worked | 700 MPa | 450 MPa | -196°C to +400°C | Food processing, pharmaceutical equipment, architectural facades. |
| Stainless A4-80 (AISI 316) | Austenitic Cr-Ni-Mo Stainless, Heavy Drawn | 800 MPa | 600 MPa | -196°C to +400°C | Marine splash zones, offshore platforms, chemical process conduits. |
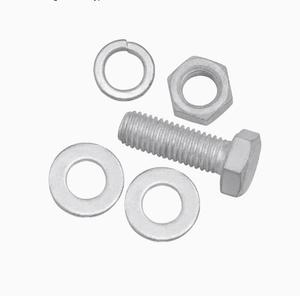
| EN 14399-4 Class 10.9 HV | High-Grade Quenched & Tempered Alloy | 1,000 MPa | 900 MPa | -50°C to +300°C | Preloaded high-strength structural bolt-nut-washer assemblies. |
Engineered answers addressing critical material compatibility, preloading calculations, hydrogen bake-out, and international export compliances.
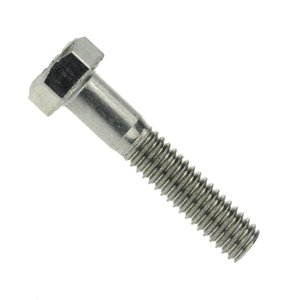
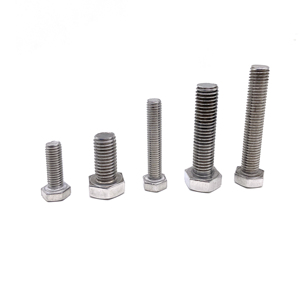
DIN 933 specifies a fully threaded shank from beneath the head to the point, ideal for tapped blind holes and high-clamping short-grip assemblies. In contrast, DIN 931 features a smooth unthreaded grip shank with a partial thread length (calculated as 2d+6mm for lengths ≤125mm). The unthreaded shoulder of the DIN 931 yields higher shear capacity across the shear plane of bolted joints.
Hydrogen embrittlement occurs during acid pickling and electro-galvanizing when nascent hydrogen migrates into steel grain boundaries under tension. For fasteners with core hardness ≥320 HV (Property Class 10.9, 12.9, and ASTM A490), we enforce mechanical blast-cleaning instead of acid pickling, mandate baking at 190°C–220°C for a minimum of 4–8 hours within 1 hour of plating, or utilize zinc-flake dip-spin coatings.
Hot-dip galvanizing adds 45–65 microns of zinc-iron alloy layer onto the threads, which would cause standard internal/external threads to seize. To maintain proper pitch clearance, bolts are threaded to standard tolerances (6g) prior to galvanizing, while mating internal nuts are overtapped after HDG dipping to 6AZ or 6AX tolerances per ISO 965-5 to guarantee free-running thread engagements.
An authentic EN 10204 3.1 MTC is issued by the manufacturer's inspection representative who is fully independent of production. It details: original raw material heat identification, chemical ladle breakdown (C, Si, Mn, P, S, Cr, Mo, Ni), tensile strength, 0.2% offset yield stress, percentage elongation, reduction of area, Charpy V-notch impact energy at designated temperatures, core/surface hardness, and dimensional sign-off.
Yes. As an OEM manufacturer, we produce custom hex head thicknesses, collar flanges, dog points, drilled cotter pin holes, and customized client head trademarks alongside required strength stamps. Production runs to customer blueprints are accommodated across carbon steels, duplex alloys, Monel, aluminum bronze, and phosphor bronze from M2 up to M100 diameters.
Preload torque is computed using the relationship T = K × D × F, where T is target torque, K is the nut friction coefficient (nut factor, which varies from 0.12 for lubricated threads to 0.22 for dry zinc), D is nominal bolt diameter, and F is specified clamp force (typically 65% to 75% of proof strength). We supply verified tightening tables and can deliver pre-lubricated PTFE or moly-coated studs for uniform torque-to-tension conversion.
Consult directly with our metallurgists and international export coordinators. Whether you require standard property class 8.8/10.9 building fasteners, EN 14399 preloaded structural sets, or custom high-nickel alloy studs for offshore pipelines, we provide verified test records, project-aligned commercial conditions, and certified manufacturing capacity.