Engineered Industrial Fasteners, High-Tensile Studs & Forged Flanges Built to ASTM, DIN & ISO Specifications for High-Stress Global Applications
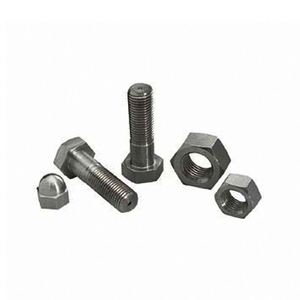
Explore our primary production lines encompassing quenched & tempered high-tensile bolts, DIN-compliant threaded rods, ANSI forged flanges, and modular accessories manufactured with controlled microstructure integrity.
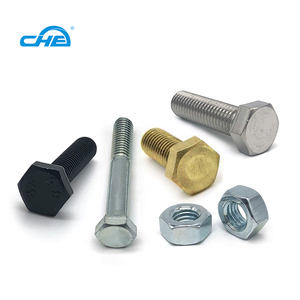
In high-load mechanical, civil, and petrochemical infrastructure, threaded rods serve as primary load-path elements subjected to cyclic fatigue, extreme shear vectors, and catastrophic tensile spikes. As an established Custom OEM Threaded Rods Manufacturer & Factory, our production paradigm bypasses conventional subtractive threading. Instead, we implement ultra-high-precision cold-roll forming up to M100 diameters. The roll-forming process plastically deforms annealed and pre-tempered alloy billets without interrupting longitudinal grain alignment, providing up to a 30% increase in fatigue yield strength compared to traditional thread-cutting techniques.
Operating under rigorous Pressure Equipment Directive (PED 2014/68/EU) accreditations and active membership within the Fastener Manufacturers Association of India (FMAI), our facilities enforce atomic-level material verification. Every batch of chromium-molybdenum alloy (ASTM A193 Grade B7/B7M) and austenitic stainless steels (304, 316, 316L, 321, and dual-phase 2205 duplex) undergoes comprehensive Optical Emission Spectrometry (OES) alongside automated ultrasonic flaw detection. This eliminates micro-inclusions before entering production lines, ensuring complete structural integrity in demanding thermal environments reaching +538°C (+1000°F) or sub-zero cryogenic down to -196°C.
| Material Standard | Base Composition | Yield Strength Min (MPa / ksi) | Tensile Strength Min (MPa / ksi) | Hardness Rating (Rockwell) | Optimum Operating Milieu |
|---|---|---|---|---|---|
| ASTM A193 Gr. B7 | AISI 4140/4142 Cr-Mo Q&T | 725 MPa / 105 ksi | 860 MPa / 125 ksi | HRC 24–35 max | High-pressure vessels, boiler piping, LNG terminals |
| ASTM A193 Gr. B8M Cl. 2 | AISI 316 Molybdenum Austenite | 655 MPa / 95 ksi | 760 MPa / 110 ksi | HRC 25–32 (Strain Hardened) | Subsea flanges, offshore splash zones, sour brine |
| ISO 898-1 Class 10.9 | Medium Carbon Boron/Alloy Steel | 900 MPa / 130 ksi | 1040 MPa / 150 ksi | HRC 32–39 | Automotive drive-trains, structural pre-tension frames |
| ASTM A320 Gr. L7 | Chromium-Molybdenum Q&T | 725 MPa / 105 ksi | 860 MPa / 125 ksi | HRC 22–32 (Charpy Tested) | Cryogenic liquified gas storage down to -101°C |
| Silicon / Aluminum Bronze | Cu-Si / Cu-Al-Ni Heavy Alloy | 380 MPa / 55 ksi | 620 MPa / 90 ksi | HRB 85–95 | High-saline shipbuilding, non-sparking valves |
Established in Mumbai in 2010, our state-of-the-art forging workshops operate fully audited Quality Management Systems certified to Pressure Equipment Directive (PED) Annex I, Paragraph 4.3 and active governance under the Fastener Manufacturers Association of India.
As one of the three largest exporters of Hot Dip Galvanized fasteners in India, our in-house automated spin-galvanizing baths deposit uniform, micro-crack-free zinc matrices strictly compliant with ASTM A153 Class C and ISO 10684, surpassing 1,500-hour neutral salt-spray benchmarks.
No bolt or threaded rod leaves our gates without an indisputable digital footprint. Every crate carries physical Mill Test Certificates detailing heat melt origins, ladle chemistry, yield-point hysteresis, Charpy V-notch impact joules, and non-destructive hydrostatic/magnetic testing data.
Traditional electro-galvanizing is rapidly being retired across marine, LNG, and petrochemical sectors due to hydrogen embrittlement risks in property classes ≥ 10.9. Global engineering procurement is gravitating toward fluoropolymer, PTFE, and zinc-nickel barrier systems (e.g., Xylan® / Geomet®) which provide zero torque-friction variance during controlled torque-tension bolting and resist prolonged chloride pitting.
Driven by European Union Carbon Border Adjustment Mechanisms (CBAM), procurement directors increasingly prioritize suppliers delivering quantifiable low-embodied-carbon fasteners. Our mills are actively transitioning forging runs to electric arc furnace (EAF) scrap feeds, alongside laser-etched 2D DataMatrix QR codes directly on rod shanks to enable immediate traceability of recycled content on construction sites.
The expansion of green liquid hydrogen (−253°C) fuel networks requires threaded connection systems that display zero ductile-to-brittle transition phenomena. Our advanced engineering laboratory is pioneering stabilized ASTM A320 Grade L7M and nitrogen-strengthened austenitic grades to service upcoming clean energy distribution grids.
Q: What is the comprehensive size and length envelope for custom threaded rods?
Our automated cold roll-forming and CNC turning centers manufacture imperial diameters from 1/4" up to 4" and metric diameters from M2 up to M100. Lengths range from standard 1,000mm, 2,000mm, and 3,000mm lengths up to continuous 6-meter threaded bars, complete with custom chamfered, dog-pointed, or tapped ends manufactured directly to CAD specifications.
Q: How do you prevent hydrogen embrittlement on property class 10.9 and 12.9 high-tensile rods?
For high-tensile steels exceeding 1000 MPa tensile strength, electro-galvanizing presents significant risks of interstitial hydrogen entrapment. We utilize precisely governed baking cycles (de-embrittlement at 190°C–220°C for 4 to 24 hours immediately post-acid pickling) or mandate mechanically deposited zinc, hot dip galvanizing with controlled fluxing, or micro-thin zinc flake coats conforming to ISO 10683.
Q: Can your factories support dual-certified materials for critical petrochemical environments?
Yes. We regularly forge and stock dual-certified fasteners, including ASTM A193 Gr. B8/B8M Class 1 and Class 2 (carbide solution treated and strain-hardened), as well as dual-grade 304/304L and 316/316L, fully aligned with NACE MR0175 / ISO 15156 guidelines for sour gas (H2S-containing) oil refinery installations.
Q: What documentation package accompanies export shipments destined for the EU, Middle East, or the Americas?
Every delivery includes full documentation containing EN 10204 Type 3.1 Inspection Certificates, heat-treatment furnace charts, 100% PMI (Positive Material Identification) spectroscopic logs, raw material melt heat references, coating thickness magnetic gauge logs, and third-party inspection releases (DNV, Lloyd's Register, BV, or TUV) whenever requested.
Whether your procurement requires urgent delivery of standard DIN 975/976 threaded rods, high-temperature ASTM A193 B7 studs, or bespoke custom forgings to unique tolerances, our engineering team is ready to analyze your drawings and bill of materials.