
Engineered for severe duty within petrochemical refining, offshore exploration, cryogenic LNG distribution, and pressure vessel manufacturing. Fully tested with Mill Test Certificates (MTC EN 10204 3.1/3.2).
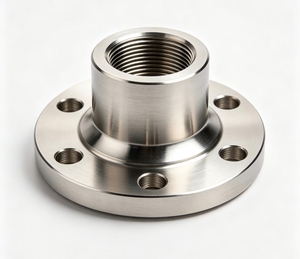
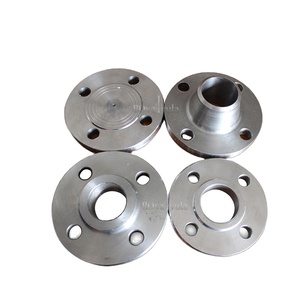
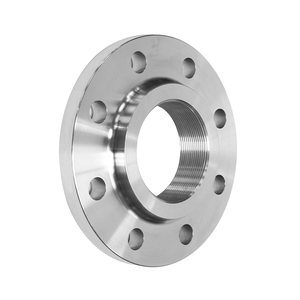
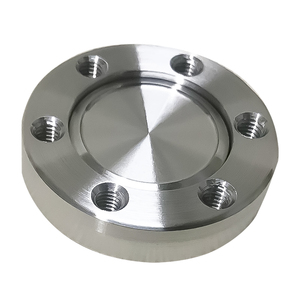
In high-pressure fluid transfer and thermodynamic piping loops, the integration of seamless butt-weld pipe fittings—such as 45°/90°/180° long-radius elbows, equal and reducing tees, concentric and eccentric reducers, and caps—eliminates structural stress concentration factors inherent in longitudinal welded seams. Fabricated according to ASME B16.9, ASME B16.28, and MSS-SP-75 standards, our seamless manufacturing methodology leverages induction mandrels and hydraulic cold extrusion to maintain consistent wall thickness across extrados and intrados geometries.
Metallurgical reliability is reinforced through normalized, quenched, and tempered heat treatments. By eradicating mechanical anisotropy and microstructural segregation, our fittings achieve exceptional Charpy V-Notch impact toughness down to -46°C (ASTM A420 WPL6) for arctic and cryogenic duties, while matching the demanding tensile thresholds required for high-yield sour gas transport under NACE MR0175/ISO 15156 guidelines.
| Material Class | Material Standards | Grade Designation | Tensile Strength (min) | Yield Strength (min) | Certifications |
|---|---|---|---|---|---|
| Carbon Steel | ASTM A234 / A105 | WPB, WPC, Gr. A105N | 415 – 585 MPa | 240 MPa | PED 2014/68/EU |
| Low-Temp Carbon | ASTM A420 / A350 | WPL6, LF2 Cl.1 | 415 – 655 MPa | 240 MPa | Charpy @ -46°C |
| Alloy Steel | ASTM A234 / A182 | WP11, WP22, WP91, F11, F22 | 585 – 760 MPa | 415 MPa | High Temp Creep |
| Austenitic Stainless | ASTM A403 / A182 | WP304/304L, WP316/316L | 485 – 515 MPa | 170 – 205 MPa | IGC Test A262 |
| Duplex & Super Duplex | ASTM A815 / A182 | S31803, S32205, S32750 | 750 – 800 MPa | 550 MPa | PREN ≥ 42 |
| Engineered Fasteners | ASTM A193 / A194 | B7/2H, B8/Gr.8, B8M/8M | 125 ksi (B7) | 105 ksi (B7) | FMAI Traceable |
Founded in 2010, our facility has expanded into a PED-approved manufacturer, FMAI member, and one of the largest exporters of hot-dip galvanized fasteners and forged pipeline assemblies globally.
Certified pressure equipment manufacturing capabilities compliant with the European Pressure Equipment Directive, enabling seamless integration into mission-critical EU and global installations.
Send an InquiryEnd-to-end forged manufacturing capacity ranging from sub-miniature instrumentation hardware up to heavy industrial M100 studs and large-diameter 48-inch seamless butt-weld pipeline components.
Send an InquiryDominant export leader in specialized Hot Dip Galvanized (HDG) coating, Fluoropolymer/PTFE coatings, and Zinc-Nickel electroplating, guaranteeing over 1,500 hours of salt spray corrosion barrier endurance.
Send an InquiryEvery single seamless fitting and forged bolt batch is issued with verified Chemical Analysis, Mechanical Tensile/Yield testing, Charpy Impact reports, and Ultrasonic / Magnetic Particle NDT certification.
Send an InquiryLongstanding member of the Fastener Manufacturers Association of India, spearheading advanced hot/cold forming methodologies, calibrated thread rolling tolerances, and stringent metallurgy controls.
Send an InquiryProven track record furnishing mission-critical pipeline fittings and structural boltings to tier-1 LNG projects, oil and gas developments across the Middle East, Far East Asia, and West Africa.
Send an InquiryStrategic insights for chief procurement officers and pipeline engineering consultants navigating decarbonization, geopolitical supply chain resilience, and digital traceability.
Transitioning toward high-pressure hydrogen transport demands seamless fittings immune to hydrogen embrittlement. Modern procurement contracts stipulate strictly controlled carbon equivalent (CE) levels (CE ≤ 0.41%), microscopic grain refinement, and tailored micro-alloying with titanium or vanadium to prevent gaseous hydrogen cracking.
Manufacturing is evolving away from energy-intensive multi-stage stamping to high-frequency induction pushing and precision cold hydro-forming. This yields tighter geometrical tolerances on ovality (within 1.0%), uniform wall reduction across the bend spine, and eliminates subsequent stress risers without unnecessary scrap.
Procurement teams are replacing paper certifications with laser-etched 2D data matrix codes directly on fittings and flange rims. These link instantly to cryptographic Mill Test Certificates, providing unalterable provenance data from raw vacuum-degassed ingot through to quenching parameters.
Deep-sea drilling and aggressive chemical refining have driven a sharp rise in standardizing nickel-chromium alloys (Inconel 625, Hastelloy C276) and Super Duplex UNS S32750/S32760 seamless fittings in regular stock programs, cutting lead times for EPC project maintenance outages from 24 weeks down to off-the-shelf dispatch.
European and American infrastructure programs increasingly require Environmental Product Declarations (EPD). Modern seamless manufacturers utilize Electric Arc Furnace (EAF) metallurgy driven by renewable power, achieving up to a 65% reduction in embedded scope 1 and 2 carbon emissions compared to traditional blast furnace routes.
To reduce expensive on-site welding costs and minimize leak pathways, global EPCs demand that seamless fittings manufacturers supply fully fabricated, pre-tested, and spool-assembled sub-systems equipped with integrated forged flanges and pre-torqued ASTM A193 B7 stud bolting.
Answers to common engineering queries regarding seamless fitting tolerances, testing regimens, weld bevel compliance, and export documentation.
Seamless fittings are forged or hot-extruded from a solid billet or seamless pipe, containing zero longitudinal or spiral weld seams. Welded fittings (such as ERW or EFW) are formed from steel plate with welded joints requiring 100% radiographic examination. Seamless fittings offer superior hoop stress distribution, eliminate heat-affected zone (HAZ) variability, and are universally specified for Class 300+ severe high-pressure, explosive hydrocarbon, and subsea pipelines.
During the mandrel hot-expansion process (Hamburg process), the parent pipe wall naturally stretches along the outer radius. We mitigate thinning by utilizing pre-engineered heavy-wall starting billets and proprietary induction temperature zoning. This guarantees that finished wall thickness across the entire extrados meets or exceeds the minimum 87.5% nominal wall thickness criteria designated under ASME B16.9 and MSS-SP-75.
Yes. While standard bevels conform to ASME B16.25 (37.5° ± 2.5° with a 1.6mm root face), automated orbital pipeline welders require compound bevels (such as J-bevels or narrow-gap 5° to 10° bevels with ultra-tight root face tolerances within ±0.2mm). All our end preps are completed on multi-axis CNC end-facing lathes to ensure zero hi-lo mismatch during field alignment.
Every production lot undergoes 100% visual and dimensional verification. Depending on contract specification, non-destructive testing includes Ultrasonic Examination (UT) of body and bevel ends per ASME Section V, Wet Fluorescent Magnetic Particle Inspection (MPI) for ferromagnetic steel, Liquid Penetrant Inspection (PT) for stainless/duplex alloys, and Positive Material Identification (PMI) using handheld XRF spectrometry to prevent material mix-ups.
Orders are dispatched with comprehensive technical dossiers including EN 10204 3.1 Mill Test Certificates (with option for third-party EN 10204 3.2 inspection by DNV, Lloyd's, or TÜV), Raw Material Ingot Traceability, Heat Treatment Charts (time vs. temperature), Hydrostatic or NDT Test Records, Hardness Surveys (Vickers/Brinell), and Certificate of Origin (COO).
Carbon and low-alloy steel fittings are pickled, passivated, and coated with quick-drying rust-preventative black bituminous lacquer or transparent anti-rust oil. Beveled ends are capped with heavy-duty polyethylene bevel protectors. Products are then wrapped in moisture-barrier VCI foil and packed into reinforced fumigated wooden crates (ISPM 15 compliant) or steel-strapped europallets.
Connect directly with our metallurgy and engineering sales teams in Mumbai. Whether you need standard schedule fittings off-the-shelf, heavy-wall extrusion custom geometries, or complete ASTM A193/A194 bolted flange assemblies with verified EN 10204 3.1 certificates, we provide rapid quotation turnaround within 24 hours.