
Explore our precision-manufactured butt weld, high-pressure swivel, investment cast, sanitary, and grooved ductile iron elbow lines calibrated for mission-critical hydraulic, petrochemical, marine, and firefighting systems.
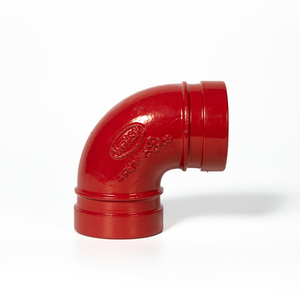
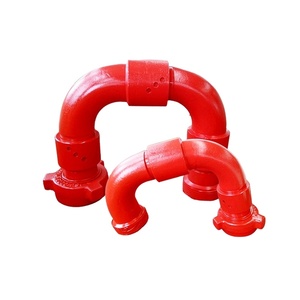
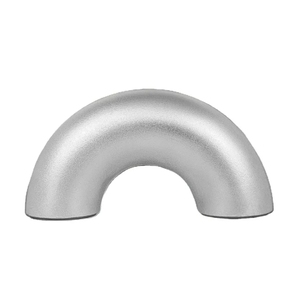
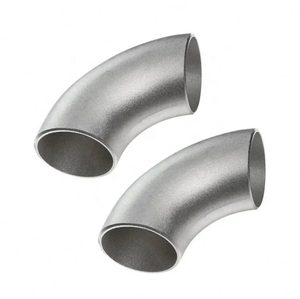
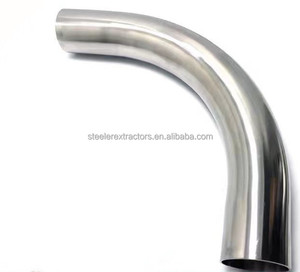
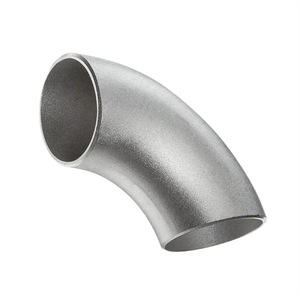
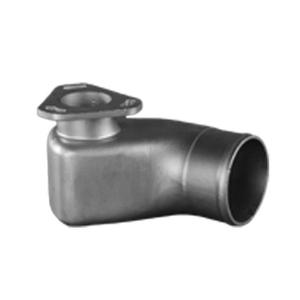
In modern process industries, oil and gas transport networks, thermal power stations, and offshore structures, the pipe elbow represents the single most stressed hydrodynamic component in any pressurized piping arrangement. Flow directional redirection introduces high turbulence, localized wall shear stresses, cavitation risks, and cyclic pressure shocks. As an industry-acclaimed China pipe elbows factory and certified global exporter, our manufacturing doctrine merges computational fluid dynamic (CFD) geometry optimization with state-of-the-art forging, extrusion, and casting technology.
Every elbow we produce—spanning ASME B16.9 butt weld elbows, heavy-duty ASTM A234 WPB carbon steel fittings, cryogenic ASTM A420 WPL6 bends, and super-duplex UNS S32750/S31803 stainless components—is manufactured under an ISO 9001 and PED 2014/68/EU compliant framework. Our production facilities maintain total heat trace integrity, meaning that every raw billet, seamless hollow, or ductile casting is backed by verifiable chemical spectroscopy and mechanical destructive testing metrics.
Utilizing high-frequency induction heating and horn-shaped mandrels, our carbon and alloy steel elbows achieve consistent wall thickness at both the intrados and extrados with uniform crystalline restructuring and minimal ovality.
Every butt weld elbow end is processed on multi-axis CNC machines to achieve precise ASME B16.25 beveling (37.5° ± 2.5° with 1.6mm root face) ensuring automated orbital root pass penetration without burn-through.
From initial ultrasonic thickness testing (UT) and magnetic particle inspection (MPI) to radiographed volumetric analysis and hydrostatic burst verification, defects are eliminated prior to ocean freight dispatch.
Procurement teams regularly balance spatial footprints with line friction loss. Our manufacturing engineering team helps EPC contractors evaluate pressure drops and flow separation risks across diverse operational contexts:
Long Radius (LR) Elbows (Center-to-Face = 1.5 × NPS): Long radius configurations are specified across refinery transport lines, offshore hydrocarbon risers, and high-velocity steam runs. The extended centerline radius dampens secondary vortex generation, drops the Moody friction factor by up to 34% compared to short radius configurations, and curtails erosive particle impingement against the back curve (extrados).
Short Radius (SR) Elbows (Center-to-Face = 1.0 × NPS): Designed strictly for compact spatial environments such as shipboard engine rooms, offshore platform modules, skids, and chemical refrigeration loops. SR elbows impose higher localized head loss and intensified fluid shear, demanding high-grade schedule ratings (SCH 80 or SCH XXS) to forestall wall erosion over extended service lifecycles.
3D, 5D, and Induction Bends: For pipeline pigging loops and slurry lines where hydraulic pressure shock and pig passage cannot tolerate abrupt curvature transitions, our induction bending lines manufacture large-radius continuous bends without intermediate circumferential welds.
This technical matrix cross-references the international design specifications, alloy classifications, heat treatments, and typical industrial destinations for our primary pipe elbow output:
| Material Standard | Applicable Grades | Manufacturing Standard | Wall Schedule Range | Standard Heat Treatment | Target Applications |
|---|---|---|---|---|---|
| ASTM A234 Carbon Steel | WPB, WPC, WP11, WP22 | ASME B16.9 / MSS-SP 75 | SCH 10 to SCH XXS (1/2" - 48") | Full Normalizing / Stress Relieved | Refineries, power generation, steam mains |
| ASTM A420 Low-Temp Steel | WPL6, WPL3, WPL9 | ASME B16.9 / EN 10253-2 | SCH 20 to SCH 160 (1/2" - 36") | Normalized & Quenched/Tempered | Cryogenic LNG systems, Arctic cross-country lines |
| ASTM A403 Stainless Steel | WP304/304L, WP316/316L, 321 | ASME B16.9 / DIN 2605 | SCH 5S to SCH 80S (1/2" - 32") | Solution Annealed (≥ 1040°C) + Water Quench | Petrochemical, offshore saline, acid handling |
| ASTM A815 Duplex Stainless | UNS S31803 (2205), S32750 (2507) | ASME B16.9 / MSS-SP 43 | SCH 10S to SCH 80S | Rapid Water Solution Annealed | Desalination plants, sour well gathering lines |
| ASTM A536 Ductile Iron | 65-45-12 / QT450-10 | AWWA C606 / FM 1920 / UL 213 | 1" to 12" Grooved Ends | Ferritizing Anneal / As-Cast High Ductility | Fire protection sprinkler loops, municipal HVAC |
| JIS SCS13 / SCS14 Cast Steel | CF8 / CF8M Equivalent | JIS B2311 / Custom OEM Molds | Investment Cast to Specification | High-Temperature Solution Treated | Marine wet exhaust, turbocharger elbows, defense |
The global piping components sector is witnessing a transformative structural realignment. Supply chain vulnerability, accelerated carbon emission taxation, and hydrogen infrastructure transitions are dramatically altering how engineering, procurement, and construction (EPC) conglomerates select manufacturing partners in China.
Global decarbonization mandates require elbows capable of handling pure H2 and hydrogen-blended natural gas without hydrogen embrittlement. Sourcing focuses on low-carbon equivalents with stringent HIC/SSCC certification per NACE TM0284.
Field manual stick welding is rapidly yielding to automated orbital root-pass welding rigs. Contractors demand elbows with razor-thin root face variations (≤ ±0.2mm) to prevent field fit-up delays and cut total installed project costs.
Tier-1 European and North American developers increasingly mandate Environmental Product Declarations (EPD). Modern factories utilizing electric induction heating instead of coal furnaces gain distinct procurement preference.
During the thermal or cold pushing of pipe elbows, tensile elongation along the outer curve (extrados) naturally induces wall thinning, while compressive stress thickens the inner throat (intrados). Historically, unscrupulous fabricators utilized thin-wall starting stock, producing elbows whose back wall dipped below the 87.5% nominal wall thickness threshold required by ASME B16.9.
Modern quality assurance mandates that buyers contractually specify starting pipe thickness ratios (typically starting at 1.15× to 1.25× nominal wall) and demand 100% multi-point ultrasonic gauge mappings along the centerline extrados. At our manufacturing plant, our specialized mandrels feature differential radius compensations that prevent thinning from exceeding 5%, preserving critical structural burst factors even under transient water-hammer spikes.
Building on over two decades of metallurgical and forging engineering heritage, our company stands among China’s foremost tier-one manufacturers and exporters of industrial steel piping products. We bridge the gap between heavy manufacturing capacity and strict international compliance.
Certified under ISO 9001, ISO 14001, ISO 45001, CE-PED 2014/68/EU, FM 1920, UL 213, and AD 2000-Merkblatt W0 for European high-pressure pressure vessel compliance.
Equipped with optical emission spectrometers (OES), Charpy V-notch impact machines down to -196°C, Brinell/Rockwell hardness testers, and hydrostatic test cells to 100 MPa.
Every elbow is rust-inhibited via phosphating, black bitumen painting, or clear varnish, capped with heavy-duty end protectors, and crated in steel-strapped ISPM-15 fumigated timber.
Traceability is the decisive factor that differentiates reputable industrial manufacturing from sub-standard commodity fittings. At our plant, no pipe elbow leaves the premises without a 100% heat-traceable Mill Test Certificate (MTC) formulated in strict accordance with EN 10204 Type 3.1 (and third-party inspected under Type 3.2 on demand by DNV, Lloyd's Register, BV, or SGS).
Our computerized continuous normalizing, quenching, and solution annealing furnaces record thermal soak profiles automatically. Each batch run is indexed to the furnace log, tracking temperature variations within ±5°C across zones. This metallurgical precision ensures that carbon steels exhibit fine-grained ferritic-pearlitic microstructures for extreme toughness, while stainless fittings achieve complete chromium carbide dissolution, mitigating intergranular sensitization during field pipeline welding.
Detailed answers to key engineering, dimensional, metallurgy, and logistics questions submitted by overseas project engineers and international buyers.
Under ASME B16.9 and referenced ASTM base standards (such as ASTM A234 or ASTM A403), the minimum wall thickness at any point on the elbow—including the extrados—must not be less than 87.5% of the nominal pipe wall thickness (equivalent to the standard mill undertolerance of -12.5%). Our manufacturing controls typically keep thinning within a tighter limit of 3% to 5% to guarantee full pressure design factor compliance.
A standard ASME B16.9 Long Radius elbow features a bend centerline radius equal to 1.5 times the nominal pipe diameter (e.g., a 10-inch LR elbow has a 15-inch radius). 3D and 5D pipe bends have radii equal to 3 and 5 times the nominal pipe size, respectively. While 1.5D elbows are compact and factory hot-pushed, 3D and 5D bends are produced on hot induction bending rigs to accommodate internal pipeline inspection gauges (PIGs) and minimize scouring in abrasive slurry or multiphase fluid services.
Every heat is tested using stationary Optical Emission Spectrometry (OES) to accurately quantify carbon (≤0.030% for L-grades), chromium, nickel, and molybdenum content. Mechanical properties are confirmed through tensile testing, elongation measurement, and Rockwell B hardness checks. Furthermore, intergranular corrosion susceptibility tests (ASTM A262 Practice E) are performed on representative post-annealing specimens.
Our grooved ductile iron elbows are manufactured from ASTM A536 Grade 65-45-12 / QT450-10 ductile iron and are fully certified by Factory Mutual (FM Approvals) and Underwriters Laboratories (UL/ULC Listed). They feature ductile elongation above 12%, a nominal operating rating of 300 to 500 PSI, and are 100% factory hydrostatically pressure-tested before epoxy powder coating or hot dip galvanizing.
Yes. In addition to standard 45°, 90°, and 180° configurations, our multi-axis CNC cold circular saws and plasma cutting systems can segment both seamless and welded elbows to any customer-specified design angle with accurate root face and bevel transitions per ASME B16.25.
Carbon steel elbows undergo exterior surface treatment consisting of black resin bitumen painting, cold electro-galvanizing, or thermal hot-dip galvanizing per ASTM A153. Stainless steel items are fully acid-pickled and passivated. All bevel ends are fitted with plastic end protectors to prevent handling ding marks, and goods are packaged in moisture-barrier lined, heavy-duty wooden crates.
For standard carbon and stainless steel elbows in nominal sizes 1/2" through 24" (SCH 40/80), we maintain an active buffer stock of over 2,000 tons with ready dispatch in 5 to 7 days. For custom heavy-wall, large-diameter (up to 48"), or special alloy orders (Duplex, Monel, Inconel), production cycles range from 20 to 35 business days. Flexible MOQs are available for project trial orders.