
Direct from manufacturing lines: engineered heavy-duty washers, flange connections, and industrial concrete anchors certified for critical mechanical assemblies.
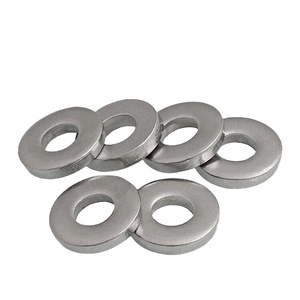
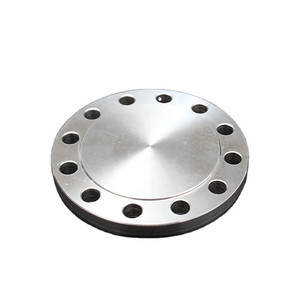
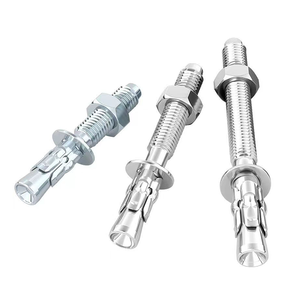
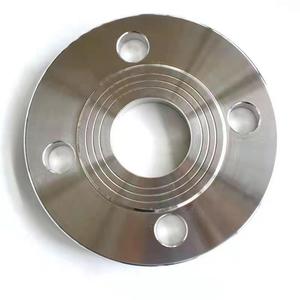
Founded in Mumbai in 2010, Viha Steel & Forging has solidified its international position as a premier, PED-approved manufacturer and global exporter of high-integrity industrial bolting, pipe flanges, and precision fasteners. Operating strictly under certified ISO 9001 and European Pressure Equipment Directive (PED 2014/68/EU) mandates, we engineer products spanning metric sizes M2 to M100 and unified inch equivalents. As an active member of the Fastener Manufacturers Association of India (FMAI), our metallurgical protocols safeguard industrial projects operating within LNG liquefaction, offshore processing, chemical synthesis, and subsea distribution.
Every single batch of stainless and high-tensile steel is tied back to primary heat numbers. We furnish genuine EN 10204 3.1 & 3.2 Inspection Certificates detailing raw material melt origins, heat-treatment cycles, and Charpy V-notch impact profiles down to cryogenic regimes.
All forgings and finished fasteners undergo rigorous Non-Destructive Testing (NDT), encompassing Ultrasonic Inspection (UT), Liquid Penetrant Testing (PT), and Magnetic Particle Testing (MT), coupled with Optical Emission Spectrometry (OES) to prevent interstitial metallurgical flaws.
Recognized among India's top three exporters of hot-dip galvanized and specialized alloy fasteners. Our dedicated centrifuge-assisted galvanizing lines provide uniform zinc coatings that surpass ASTM A153/ISO 10684 guidelines without causing thread overtapping degradation.
Direct comparative benchmarks between standard austenitic stainless grades and high-tensile alloy bolt assemblies for severe service conditions.
| Material Specification | Tensile Strength (Min) | Yield Strength (Min) | Hardness Profile | Primary Industrial Use-Case |
|---|---|---|---|---|
| ASTM A193 Gr. B8 (SS 304 Class 1) | 75 ksi (515 MPa) | 30 ksi (205 MPa) | HRB 90 Max | Cryogenic pressure vessels, food manufacturing, nitric acid environments. |
| ASTM A193 Gr. B8M (SS 316 Class 2) | 110 ksi (760 MPa) | 95 ksi (655 MPa) | HRC 25–32 | Offshore platform bolting, marine heat exchangers, chloride pipeline assemblies. |
| ASTM A193 Gr. B7 (Alloy 4140 Q&T) | 125 ksi (860 MPa) | 105 ksi (720 MPa) | HRC 35 Max | High-pressure, high-temperature steam headers and refinery catalytic crackers. |
| EN 14399-4 Class 10.9 HV | 1000 MPa | 900 MPa | HRC 32–39 | High-strength structural preloaded assemblies, bridge girders, wind turbines. |
| Austenitic A4-80 Stainless Steel | 800 MPa | 600 MPa | HRB 95 Min | Desalination plants, marine topsides, and subsea manifolds subject to uniform pitting. |
Strategic supply chain transitions steering global EPCs, Tier-1 plant constructors, and procurement executives through 2026–2030.
With the full implementation of the European Carbon Border Adjustment Mechanism (CBAM), procurement directors require authenticated cradle-to-gate verified Carbon Intensity declarations for all exported stainless stock.
International buyers are reducing intermediate third-party distribution costs by sourcing directly through Western India's integrated manufacturing corridors, shortening lead times via direct Nhava Sheva maritime routes.
High-specification bolting packages now demand integrated QR-linked laser etching on fastener heads, granting immediate field inspectors access to chemical spectrometry maps and mill certifications.
Accelerating investments in hydrogen transport, geothermal loops, and offshore wind turbines are driving widespread demand toward UNS S32750/S32760 Super Duplex and Nickel Alloys (Inconel 625/718).
Technological refinements reshaping fastener durability, thread fatigue life, and multi-decade corrosion barriers.
Eliminating traditional thread cutting, our precision thread cold-rolling process post solution-annealing maintains unbroken grain-flow lines. This eliminates micro-notch stress concentrators and delivers a 300% extension in mechanical fatigue resistance under dynamic, vibrating environments.
To combat galvanic interaction between dissimilar metals in marine environments, we apply advanced fluoropolymer coatings (Xylan 1070 / 1024) and non-electrolytic zinc flake (Geomet). These surface applications withstand up to 3,000+ hours in ASTM B117 salt spray testing without seizing.
Our austenitic B8/B8M Class 1 studs are formulated for extreme cryogenic temperatures down to -196°C (-320°F) for liquid nitrogen and LNG storage, maintaining excellent impact ductility and zero embrittlement phase transitions over decades of cycling.
Clear, technical clarifications regarding standards, manufacturing capabilities, certification compliance, and export logistics.
Class 1 bolts are carbide-solution treated (annealed), offering superior chemical corrosion resistance but lower tensile strength (75 ksi min). Class 2 bolts undergo strain hardening (cold working) after annealing, increasing minimum tensile strength up to 125 ksi depending on diameter, making them suitable for high-stress structural joints.
Every consignment is accompanied by an authenticated EN 10204 Type 3.1 Mill Test Certificate (MTC). This documents chemical composition (Spectro Analysis), mechanical performance (yield, tensile, elongation, hardness), heat treatment records, NDT reports, and dimensional inspection sign-offs.
Galling occurs when friction shears the protective chromium oxide film. We eliminate this by utilizing tight precision pitch tolerances, pairing differing hardness levels between mating bolts (e.g., A193 B8) and nuts (A194 Gr. 8 with specialized hardness), and offering factory-applied MoS2, PTFE, or anti-seize dry lubricants.
Our manufacturing lines cover metric sizes from M2 through M100 and imperial unified threads from 1/4" up to 4" diameter. Furthermore, we maintain hot forging capabilities to create custom-length studs, special flange profiles, and draw-to-print non-standard geometries in specialized bronze, copper, titanium, and nickel alloys.
Standard stock specifications ship within 7–10 days, while custom hot forgings require 3–4 weeks. All sea freight exports are secured in moisture-resistant VCI paper, boxed in heavy-duty Euro-pallets with poly-wrap shrink strapping, and labeled with containerized barcoding to protect threading across ocean transits.
Submit your project specifications, custom drawings, or immediate stock requirements. Our engineering team provides complete quotation files, MTC samples, and compliance sheets within 24 business hours.