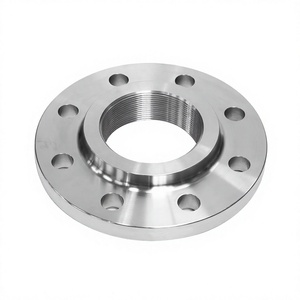
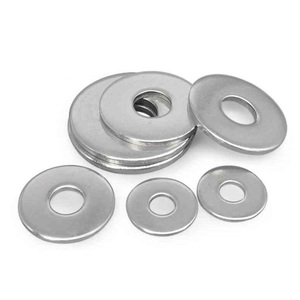
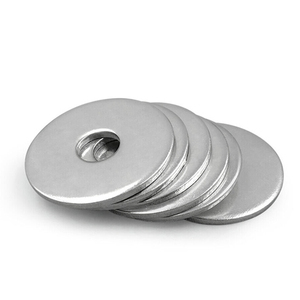
Beyond our certified U-bolt manufacturing lines, we engineer and stock complete companion hardware, heavy hex nuts, precision washers, and industrial forged flanges tested for severe petrochemical and civil environments.
Industrial U-bolts are far more than bent metal rods; they are critical static restraint systems engineered to balance dynamic thermal expansion, lateral mechanical thrust, and high-amplitude acoustic vibrations in pressurized piping networks. At our Mumbai manufacturing plant, Viha Steel & Forging combines metallurgical forging heritage with computerized bending algorithms to fabricate both round bend (DIN 3570 Type A), grip-type (DIN 3570 Type B), and square bend configurations that eliminate micro-fissures and residual stress concentrations along the radius crest.
When securing process lines across LNG carriers, offshore rigs, and chemical synthesis units, standard fasteners frequently experience stress corrosion cracking (SCC) or galling. Our factory mitigates these catastrophic failure modes through induction cold-drawing and precision hot-forging, followed by computer-regulated stress-relief annealing. Whether your application requires high-tensile chrome-moly alloy steel for elevated temperature petrochemical manifolds or cryogenic-grade austenitic stainless steel, our fully equipped forging line handles nominal diameters from M6 up to M100 (1/4" through 4" imperial) with thread tolerance classes adhering strictly to 6g and UNC 2A/2B fits.
Compare chemical compositions, tensile limits, and environmental resistances to optimize mechanical specifications for offshore platforms, refinery piping, and severe civil infrastructure.
| Steel Grade / Standard | Base Metallurgy | Tensile Strength (Min) | Yield Strength (Min) | Elongation (%) | Impact Toughness (Charpy V) | Typical Service Environment |
|---|---|---|---|---|---|---|
| ASTM A193 Grade B7 | AISI 4140/4142 Cr-Mo Alloy | 125 ksi (860 MPa) | 105 ksi (720 MPa) | 16% min | ≥ 40 J at -20°C | High-temperature, high-pressure refinery lines • Steam manifolds |
| ASTM A320 Grade L7 | Quenched & Tempered Cr-Mo | 125 ksi (860 MPa) | 105 ksi (720 MPa) | 16% min | ≥ 27 J at -101°C | Cryogenic LNG systems, Arctic midstream piping • Gas decompression |
| ISO 898-1 Class 8.8 | Medium Carbon Boron-Treated | 800 MPa | 640 MPa | 12% min | ≥ 30 J at -20°C | Heavy vehicular chassis, modular pipe racks, general structural joints |
| ISO 898-1 Class 10.9 | Alloy Steel Quenched & Tempered | 1040 MPa | 940 MPa | 9% min | ≥ 20 J at -40°C | High-stress preloaded structural connections, vibratory machinery mounts |
| ASTM A193 Gr. B8 (SS 304) | Austenitic 18-8 Stainless (AISI 304) | 75 ksi (515 MPa) | 30 ksi (205 MPa) | 30% min | High ductile retention at -196°C | Water treatment plants, clean steam, pharmaceutical, architectural |
| ASTM A193 Gr. B8M (SS 316) | Molybdenum-Enhanced 316 Austenitic | 75 ksi (515 MPa) | 30 ksi (205 MPa) | 30% min | Excellent cryogenic toughness | Marine splash zones, desal units, chloride-laden chemical exhausts |
| UNS S31803 (Duplex 2205) | 22Cr-5Ni-3Mo-0.16N Ferritic/Austenitic | 655 MPa | 450 MPa | 25% min | ≥ 80 J at -40°C | Deepwater subsea trees, sour gas scrubbers, offshore platform risers |
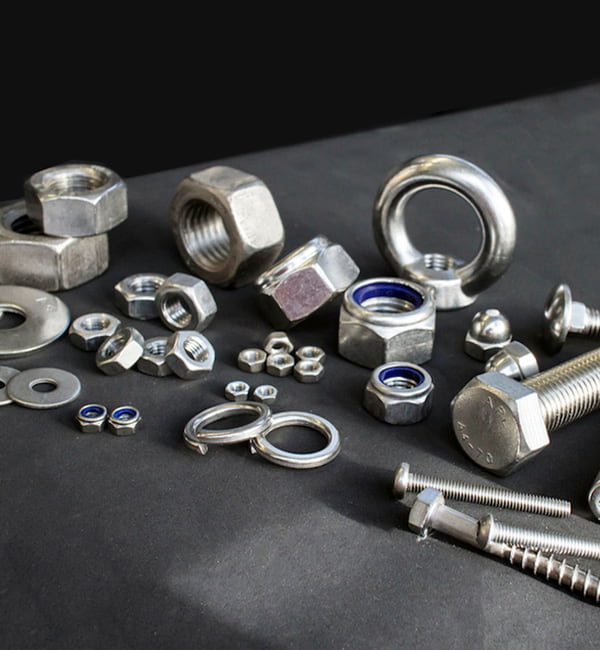
U-bolts installed outdoors or in marine coastal processing plants face severe electrochemical degradation. As the 3rd largest exporter of hot-dip galvanized fasteners in India, Viha Steel & Forging integrates proprietary chemical immersion fluxing and temperature-controlled molten zinc bath dipping (450°C–460°C) following ASTM A153 Class C and ISO 10684 specifications. This process generates intermetallic iron-zinc metallurgical bond layers (Gamma, Delta, and Zeta phases) capped by pure zinc (Eta phase), ensuring self-healing sacrificial galvanic defense exceeding 1,500 hours of neutral salt spray testing (ASTM B117) without red rust formation.
For subsea manifolds and offshore petrochemical platforms where hot dip galvanizing could lead to thread interference on close-tolerance nuts, we supply fluoropolymer thermoset coatings (Xylan® / PTFE 1070) over zinc-nickel or zinc phosphate underlayers. This multi-tier coating guarantees an extraordinarily low friction coefficient (μ = 0.08–0.12), ensuring predictable torque-tension relationships, preventing galling during high-speed torque wrenching, and resisting chemical exposure across a broad thermal range of -250°C to +260°C.
Procurement teams and EPC project managers face shifting global dynamics. Here is how advanced metallurgical fabrication and smart supply chain governance are redefining industrial fastener sourcing.
Modern EPC contractors are transitioning away from buying raw U-bolts, washers, and hex nuts as detached line items. The rising global standard calls for fully tagged, pre-assembled kits featuring matched DIN 934 / ASTM A194 nuts, vulcanized neoprene isolation pads, and locking Belleville spring washers. Pre-assembly on our factory floor reduces field staging labor by up to 45% and eliminates thread cross-matching errors on site.
Rather than procuring entry-level zinc-plated carbon steel that demands replacement within 24 to 36 months, global operators in West Africa, the Middle East, and Southeast Asia are standardizing on duplex stainless steels (2205 / 2507) and Super Austenitic 904L. Upfront material premiums are amortized within 3 years through eliminated plant shutdowns, minimal scaffolding erection, and zero hydrocarbon line leakages.
International decarbonization mandates require measurable Scope 3 emissions reporting across capital equipment. Viha Steel & Forging partners with premier electric-arc furnace (EAF) mills utilizing direct reduced iron (DRI) and recycled ferrous scrap. Each production batch includes audited product carbon footprints alongside mechanical EN 10204 3.1 certification, satisfying ESG audit benchmarks in Europe and North America.
In critical structural and pressure vessel engineering, fastener reliability is non-negotiable. Viha Steel & Forging operates an ISO 9001:2015 accredited laboratory and maintains formal Pressure Equipment Directive (PED 2014/68/EU) certification. As an active corporate member of the Fastener Manufacturers Association of India (FMAI), our Mumbai plant enforces an uncompromising 8-stage inspection loop before any crate leaves for export.
Incoming steel billets undergo optical emission spectroscopy (OES) to verify carbon, sulfur, phosphorus, and micro-alloy concentrations. During thread-rolling and cold-heading stages, optical profile comparators continuously check thread pitch, root crest radius, and thread angle. After quenching and tempering, each lot undergoes Vickers and Rockwell hardness testing, proof load validation, Charpy impact testing down to cryogenic temperatures (-196°C), and wet fluorescent magnetic particle inspection (MPI) to detect any internal micro-voids or surface seams. Every shipment is accompanied by an authentic Mill Test Certificate (MTC) conforming to EN 10204 3.1 / 3.2.
Key technical answers covering dimensional standards, galvanic isolation, coating allowances, and export freight protocols.
DIN 3570 Type A features standard round bends intended for direct pipe suspension and clamping where some lateral movement from thermal expansion is permitted. DIN 3570 Type B is a grip-style assembly fitted with an integrated steel saddle support, designed to securely anchor the pipe to structural steel channels, completely locking both axial and lateral movement.
Hot-dip galvanizing adds 45 to 65 microns of protective zinc alloy. To ensure smooth thread engagement without binding or stripping the zinc, companion hex nuts (such as ASTM A563 Grade DH or DIN 934) are tapped oversize per ASTM A563 Table 1 / ISO 965-5 (6AZ or 6AX tolerances) after galvanizing, followed by corrosion-inhibiting oil lubrication.
Stainless steel alloys form a transparent chromium oxide passivating layer that can cold-weld under tightening friction. We eliminate galling by maintaining precise cold-rolled thread root geometries, providing Class 2B/6g loose fits, and applying factory-baked molybdenum disulfide (MoS2), PTFE coatings, or anti-seizing wax compounds directly onto the fastener threads.
Yes. Beyond standard DIN 3570, ASME B18.31.5, and BS 3974 configurations, we fabricate custom square U-bolts for box girders, J-bolts, eye bolts, and custom radius clamps up to M100 in carbon steel, chrome-moly, Inconel 625, Hastelloy C276, and titanium. Simply share your CAD drawing or dimensional schedule with our sales desk.
Every export shipment includes a certified EN 10204 3.1 Mill Test Certificate featuring full chemical heat analysis, actual yield and tensile test results, elongation percentage, Charpy V-notch impact values, surface coating thickness reports (ASTM B499), and non-destructive examination (NDE) release forms. Third-party inspections (Lloyd's, DNV, TÜV, Bureau Veritas) are routinely facilitated.
To prevent transit thread bruising and salt spray moisture exposure, threaded legs are protected by heavy-wall plastic mesh sleeves, bundled in high-strength polypropylene wraps with silica gel desiccant packs, and packed into fumigated ISPM-15 compliant wooden cases or steel-strapped Euro pallets with exterior waterproof barrier linings.
Whether you need a full bill-of-materials takeoff for an oil & gas pipeline, custom DIN 3570 U-bolts in special alloys, or hot dip galvanized structural bolts shipped under PED compliance, our Mumbai technical desk is ready to provide engineering support and competitive factory direct quotations.
Contact Us