Manufactured under PED 2014/68/EU certification and rigorous metallurgical standards, our core product series delivers full compatibility with Japanese Industrial Standards (JIS) and international ASME/ASTM architectures across Osaka Bay's critical infrastructures.
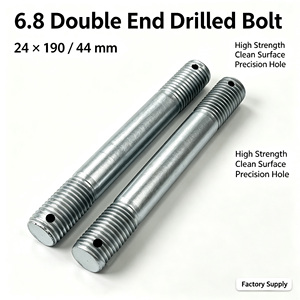
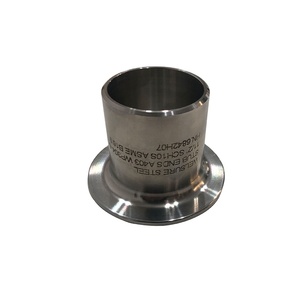
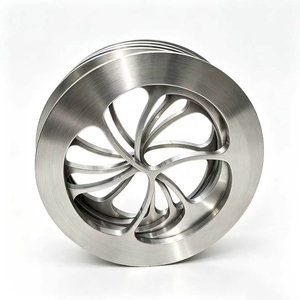
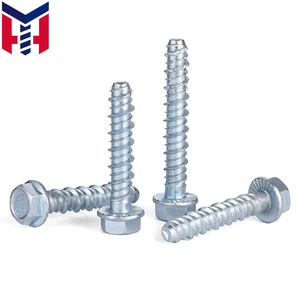
The Hanshin Industrial Region, spanning the economic powerhouses of Osaka and Hyogo Prefectures, represents Japan’s premier manufacturing and processing heartland. Centered around the strategic deep-water maritime infrastructure of Osaka Bay and the vast petrochemical and refining cluster of the Sakai-Senboku Coastal Industrial Zone, this industrial biome demands unprecedented metallurgical integrity, stringent dimensional tolerances, and airtight compliance with the High Pressure Gas Safety Act of Japan (KHK - Koatsu Gas Hoan Kyokai). Butt weld pipe fittings—encompassing long-radius elbows, equal and reducing tees, concentric and eccentric reducers, caps, and lap-joint stub ends—serve as the continuous pressure boundary for hazardous fluids, cryogenic liquefied natural gas (LNG), clean hydrogen vectors, superheated steam, and corrosive chemical streams.
For engineering procurement executives, Japanese general trading firms (sogo shosha), and EPC contractors operating across Kansai, sourcing butt weld pipe fittings and accompanying flange and fastener packages necessitates bridging international design codes (ASME B16.9, ASTM A234, ASTM A403, ASTM A420) with domestic Japanese Industrial Standards (JIS B2311 for regular carbon steel, JIS B2312 for alloy and high-pressure carbon steel, and JIS B2313 for plate-welded fittings). Viha Steel & Forging (established in 2010), a distinguished PED 2014/68/EU certified manufacturer and active member of the Fastener Manufacturers Association of India (FMAI), supplies high-integrity butt weld fittings, forged flanges, and heavy industrial bolting solutions explicitly calibrated for the rigorous operating conditions and seismic vulnerability criteria characteristic of the Osaka market.
Osaka’s strategic industrial facilities operate under severe mechanical fatigue, marine atmospheric salinity, thermal cycling, and seismic stress demands.
In the vast refinery belts of Sakai and Takaishi, our seamless ASTM A234 WPB and WP11/WP22 chrome-moly butt weld elbows provide uninterrupted hydrocracker and ethylene furnace loop service. Operating at temperatures exceeding 540°C under severe catalytic abrasion, these components maintain grain continuity and strict wall thickness margins conforming to METI ministerial ordinances.
Cryogenic storage and regasification hubs at Senboku LNG terminals require ASTM A420 WPL6 and forged stainless steel WP304L/316L stub ends and reducers. With mandatory Charpy V-notch impact testing verified down to -46°C and -196°C, our fittings prevent catastrophic brittle failure in low-boiling boil-off gas (BOG) compressor re-liquefaction lines.
Serving northern Osaka's biomedical corridors in Suita and Kansai Science City, we supply high-purity ASTM A403 WP316L orbital weld fittings with mechanically polished and electro-polished interior finishes (Ra ≤ 0.25 µm). These fittings eliminate bacterial stagnation, galvanic corrosion, and particulate contamination in ultra-pure water (UPW) and CIP systems.
1. Osaka Bay Clean Hydrogen and Ammonia Energy Hub: In alignment with Japan’s Green Growth Strategy and the Kansai Economic Federation’s clean transition roadmap, the Port of Osaka is executing ambitious demonstration infrastructure for ammonia co-firing and cryogenic liquid hydrogen import bunkering. The shift toward handling liquefied hydrogen at -253°C introduces extreme metallurgical embrittlement risks. Sourcing austenitic stainless steels with tightly controlled delta ferrite contents (<0.5% or per special cryogenic de-ferritization) and tight interstitial nitrogen stabilization has emerged as a top purchasing criterion.
2. Resilience Engineering for the Nankai Trough Megathrust Preparedness: The Osaka Prefectural Government enforces comprehensive seismic retrofit codes across coastal industrial installations. Traditional piping junctions subjected to ground displacement during seismic oscillations experience severe localized bending moments. Butt welded piping circuits, when manufactured with fully verified ductile properties and precise ovality control (≤1.0% out-of-roundness), provide significantly superior elastic-plastic deformation absorption compared to threaded or mechanical slip-on connections.
3. Rigorous Material Traceability & Non-Destructive Examination (NDE): High-pressure steam turbine renovations and industrial boiler repowering projects across Osaka and Amagasaki demand exhaustive quality verification. Japanese QA auditors mandate 100% PMI (Positive Material Identification), ultrasonic testing (UT) of raw parent pipe materials to prevent laminar shearing, and continuous hydrostatic testing.
Cross-comparative analysis for plant engineers coordinating global EPC specifications with domestic Japanese statutory mandates.
| Product Category | ASME / ASTM Standard | Equivalent JIS Standard | Common Material Grades | Nominal Size & Wall Thickness | Osaka Primary Industry Usage |
|---|---|---|---|---|---|
| Seamless Butt Weld Elbows (45°/90°/180°) | ASME B16.9 / ASTM A234 | JIS B2311 / JIS B2312 | WPB, WPC, PT370, PT410 | 1/2" to 36" (SCH 10 to SCH XXS) | Petrochemical distillation, high-pressure steam distribution |
| Equal & Reducing Tees | ASME B16.9 / ASTM A403 | JIS B2312 / JIS B2313 | WP304/304L, WP316/316L, SUS304/316 | 1/2" to 24" (SCH 5S to SCH 80S) | Refinery headers, marine chemical tankers, LNG bunkering |
| Concentric & Eccentric Reducers | ASME B16.9 / ASTM A420 | JIS B2312 (Cryogenic class) | WPL6, WPL3, SLPL | 3/4" x 1/2" to 30" x 24" (All SCH) | Centrifugal pump suction/discharge, cryogenic compressor piping |
| Lap Joint Stub Ends (Type A/B) | ASME B16.9 / MSS SP-43 | JIS B2312 / JIS B2220 compatibility | WP316/316L, WP321, Duplex S31803 | 1/2" to 16" (SCH 10S, 40S) | Frequent disassembly lines, pharmaceutical batch reactors |
| Forged Steel Flanges (WN, BL, SO) | ASME B16.5 / ASTM A105 | JIS B2220 (5K, 10K, 20K, 30K) | A105, A350 LF2, SF440A, SUSF316 | 1/2" to 48" (Class 150 to 2500#) | Pressure vessel nozzles, terminal pipeline manifolds |
| High-Tensile Flange Studs & Nuts | ASTM A193 / A194 | JIS B1180 / JIS B1181 | B7/2H, B8/Gr.8, B8M/Gr.8M, 10.9 HV | M2 to M100 (1/4" to 4" Imperial) | High-temperature heat exchanger shells, offshore platforms |
Operating an advanced manufacturing infrastructure in Mumbai, India, we ship certified pressure boundary solutions to world-class industrial hubs across Japan and the Asia-Pacific.
Using hot mandrel pushing and cold hydraulic drawing techniques, our seamless butt weld elbows and tees maintain uncompromised grain structure, zero internal wrinkles, and strictly controlled circularity.
Calibrated computer-controlled furnaces execute normalizing, quenching & tempering, and complete austenitic solution annealing at 1050°C–1150°C, followed by rapid water quenching to eradicate carbide precipitation.
100% in-house chemical verification via optical emission spectroscopy, Niton XRF positive material identification (PMI), hydrostatic pressure testing, ultrasonic lamination checks, and radiography on critical weldments.
Every single component is die-stamped with heat number, schedule, material grade, and standard. Shipped with fully certified EN 10204 Type 3.1 Mill Test Certificates (with 3.2 available on third-party witness inspection).
In-depth technical answers addressing the practical, regulatory, and logistics requirements of Kansai plant managers, EPC engineers, and procurement directors.
Compliance with the High Pressure Gas Safety Act requires exhaustive documentation confirming chemical composition, yield/tensile strength, elongation, and charpy impact energy values. Viha Steel & Forging supplies butt weld fittings accompanied by authentic EN 10204 Type 3.1 Mill Test Certificates directly cross-referenced to ladle melt heat batches. On demand, we facilitate third-party inspection audits (TUV, Lloyd’s Register, DNV, BV) to fulfill Type 3.2 certification, enabling turnkey verification by METI-accredited regional inspectors in Osaka.
Yes. We frequently manufacture dual-certified fittings engineered to bridge metric JIS dimensions and standard ASME schedules. For example, our stainless steel elbows and tees are produced to meet both ASTM A403 WP316/316L and JIS SUS316/316L chemistry and mechanical properties, with dimensional bevels machined in accordance with either ASME B16.25 (37.5° ± 2.5°) or JIS standards as designated in project drawings.
For carbon steel butt weld fittings installed within 5 km of Osaka Bay (such as Yumeshima, Nanko, or Sakai port areas), chloride atmospheric attack is severe. We provide high-performance surface protective systems: Hot Dip Galvanization conforming to ASTM A153 / ISO 1461, inorganic zinc silicate primers, fluoropolymer PTFE / Xylan coatings for bolting packages, and black oxide rust-preventative dipping for internal warehouse storage prior to project installation.
Ocean freight from Nhava Sheva Port (JNPT, Mumbai) to the Port of Osaka (Nanko Container Terminal) operates on frequent weekly direct and transshipment container liner services, typically taking 18 to 24 days. Every export consignment is packaged in ISPM-15 heat-treated, fumigated seaworthy wooden cases with heavy-duty desiccants and vapor corrosion inhibitor (VCI) bags to ensure zero moisture contamination during tropical sea transit.
As an established industrial fastener and flange manufacturer (from M2 up to M100 studs, carriage bolts, structural bolts, and anchor systems), Viha Steel & Forging provides complete bundled piping packages. EPC buyers eliminate matching errors by receiving ASTM A193 B7/B8/B8M studs paired with ASTM A194 2H/Gr.8/Gr.8M nuts, forged ASTM A105 / A182 flanges, and butt weld fittings within a single shipment under unified quality assurance documentation.
Dimensional precision is enforced using calibrated vernier height gauges, internal dial bore gauges, and coordinate measurement tools. Butt weld ends are machined to tight tolerances for wall thickness (within ±12.5% per ASME B16.9 or tighter client specification) with root face dimensions strictly held to 1.6 mm ± 0.8 mm. This guarantees smooth orbital welding fit-up and minimizes root-pass burn-through for Kansai welding teams.
Partner directly with an established PED-approved manufacturer. Send your bill of materials (BOM), project piping schedules, custom drawings, or emergency maintenance specifications to our international engineering desk.