Certified, mill-tested high-tensile connection assemblies engineered for extreme pressure containment, sour service, and structural integrity across Caspian offshore platforms and midstream export terminals.
The Caspian Sea basin represents one of the world's most intricate operating terrains for industrial piping systems, offshore production platforms, and hydrocarbon transportation corridors. As a premier Chinese manufacturing partner and high-volume exporter supplying butt weld fittings, forged flanges, and mechanical bolting hardware to the Republic of Azerbaijan, our production methodologies directly address the structural, thermodynamic, and corrosive complexities inherent to this geography.
Piping systems routed through offshore blocks such as Azeri-Chirag-Gunashli (ACG) and deep-water gas reservoirs like Shah Deniz operate under dual stress factors: elevated internal operational pressures coupled with corrosive external marine microclimates characterized by fluctuating salinity and hyperbaric conditions. In butt weld fittings—ranging from long radius (LR) and short radius (SR) 90-degree elbows to concentric and eccentric reducers, equal tees, and end caps—metallurgical stability is non-negotiable. Standard industrial grade carbon steel frequently fails under the mechanical stress of cyclical pulsating flow rates and low-temperature transition spikes prevalent in the Caucasus region.
Our export portfolio implements strict adherence to ASTM A234 WPB/WPC, low-temperature ASTM A420 WPL6, and duplex stainless grades (UNS S31803 / S32750), processed with controlled normalizing or quenching and tempering cycles. This precise heat treatment refines the grain boundary structure, lowering ductile-to-brittle transition temperatures (DBTT) well below minus 46 degrees Celsius. Consequently, our butt weld components deliver superior Charpy V-notch impact values, ensuring seamless integration with trunkline segments connected to the South Caucasus Pipeline (SCP) and the Baku-Tbilisi-Ceyhan (BTC) mainline network.
From shallow-water wellhead platforms to high-throughput petro-refining complexes in the Absheron Peninsula, our mechanical piping assets and fasteners are deployed across high-integrity nodes.
Butt weld fittings manufactured from ASTM A420 WPL6 and forged ASME B16.5 high-pressure flanges provide permanent, leak-proof joints on semi-submersible rigs and tension-leg production decks subjected to wave dynamics and offshore wind shears.
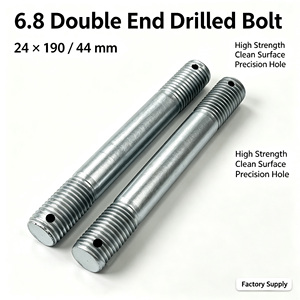
Extensive retrofitting and desulfurization initiatives demand high-alloy Cr-Mo fittings (ASTM A234 WP11, WP22) alongside ASTM A193 B7 stud bolts and heavy hex nuts capable of resisting high-temperature hydrogen attack (HTHA) and sulfurous stress crack propagation.
Continuous pipeline throughput at the Sangachal compression terminal relies on heavy-wall butt weld elbows and tees (MSS-SP-75 WPHY 52 to 70) capable of withstanding turbulent hydrodynamic friction and erosion caused by unrefined crude and gas condensates.
Market dynamics across Baku, Sumgait, and Ganja are evolving rapidly, driven by infrastructure diversification, stricter environmental emissions standards, and the Middle Corridor expansion.
As drilling moves toward deeper horizon strata within the Caspian basin, crude and natural gas streams show heightened hydrogen sulfide (H2S) concentrations. Azerbaijani EPCs and operators now enforce mandatory NACE MR0175 / ISO 15156 compliance. This requires Chinese butt weld fittings and matching forged flanges to undergo stringent hardness limitation testing (HRC ≤ 22) and Calcium Treatment for Sulfide Inclusions, preventing Hydrogen Induced Cracking (HIC) and Stress Corrosion Cracking (SCC).
The expansion of the Baku International Sea Trade Port at Alat as a pivotal nexus of the Trans-Caspian International Transport Route (TITR) is driving massive demand for structural fasteners, concrete wedge anchors, and pipe connection hardware. Port expansion, bulk liquid terminals, and bunkering facilities require hot dip galvanized fasteners, ASTM A490 structural assemblies, and heavy-duty swivel joints designed for severe atmospheric salinity and mechanical vessel berthing loads.
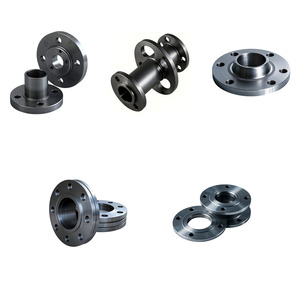
Sumgait Chemical Industrial Park (SCIP) continues to expand its downstream polymer, nitrogen fertilizer, and chemical processing capacities. This shift has elevated the consumption of corrosion-resistant austenitic (AISI 304L, 316L) and nickel-alloy piping components. Local purchasing teams are shifting from traditional fragmented procurement toward consolidated sourcing bundles that encompass seamlessly beveled butt weld reducers, ANSI B16.5 raised face weld necks, and complete Grade 8.8/10.9 structural bolting sets.
Clear, definitive answers addressing regulatory compliance, cross-standard compatibility, mill documentation, and logistics corridors between China and the Port of Baku.
Major infrastructure projects in Azerbaijan frequently integrate legacy Soviet systems governed by GOST 17375 / 17378 with modern Western modules designed per ASME B16.9 and ASME B31.3. We manufacture dual-certified and custom-dimensioned transition butt weld fittings. These feature tapered machining transitions and wall-thickness matching to ensure proper circumferential alignment, root pass weld penetration, and radiographic testing (RT) compliance across mixed piping schedules.
Every shipment is accompanied by an EN 10204 3.1 Mill Test Certificate (MTC) providing complete traceability from the electric arc furnace heat number to the final beveled component. The MTC explicitly details chemical spectrometry (including Carbon Equivalent CE values), yield and tensile mechanical test results, Charpy V-notch impact values at specified design temperatures, hardness ratings, non-destructive testing (NDT/UT/MT) results, and heat-treatment charts.
Cargo passing through maritime routes or rail links across Central Asia experiences significant thermal shifts and relative humidity swings. Our carbon steel butt weld fittings receive high-grade black anti-corrosion paint, synthetic transparent resin vanish, or specialized rust-inhibitive oil coatings. Machined beveled ends are protected by high-density polyethylene (HDPE) end protectors, and structural bolts are available with Hot Dip Galvanizing (HDG) per ASTM A153 or multi-layer zinc flake coatings.
Yes. Our manufacturing facilities operate heavy-tonnage hydraulic hot forming presses, mandrel bending equipment, and computer-controlled bevelling machines. We routinely fabricate seamless butt weld fittings up to 48 inches with wall thicknesses reaching Schedule 160, XXS, or bespoke calculated thicknesses per ASME Section VIII Division 1 guidelines for secondary recovery water and gas injection wells.
Combining profound metallurgical heritage, PED-accredited quality assurance, and end-to-end industrial supply chain integration.
Operating under rigorous Pressure Equipment Directive (PED) manufacturing guidelines and ISO 9001 certified protocols, our forging, heat treatment, threading, and machining processes are managed entirely in-house. We source steel round bars and seamless pipe billets exclusively from Tier-1 audited mills, eliminating counterfeit raw materials and ensuring metallurgical homogeneity.
Unlike singular-focus fabricators, our manufacturing scope bridges industrial pipe fittings, ASME B16.5 forged flanges, and high-tensile structural fasteners (ASTM A193 B7/B8/B8M, A325, A490, DIN 6921). This allows project buyers to consolidate entire piping packages into coordinated container shipments, reducing customs handling overhead at Baku checkpoints.
Leveraging direct intermodal railway logistics running along the China-Central Asia-West Asia economic corridor, we ensure rapid freight delivery to Baku, Alyat, and inland receiving terminals. Our specialized seaworthy export packaging uses heat-treated, fumigated timber frames, internal vapor barrier lining, and reinforced banding to guarantee zero transit deformation.
Access full dimensional tables, metallurgical specification sheets, and competitive wholesale pricing for seamless butt weld fittings, forged flanges, and high-tensile bolting packages.
Get Catalog