
Complete batch traceability with heat numbers marked directly onto forged forgings and threaded assemblies, delivered straight to industrial sites across Hai Phong, Quang Ninh, and Ba Ria-Vung Tau.
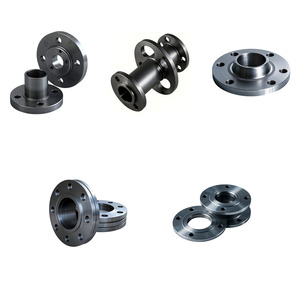
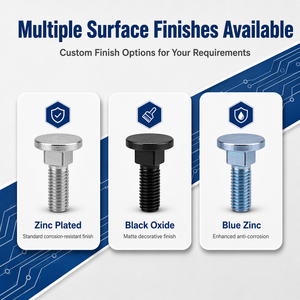
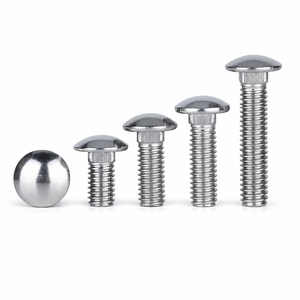
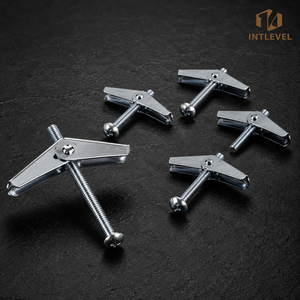
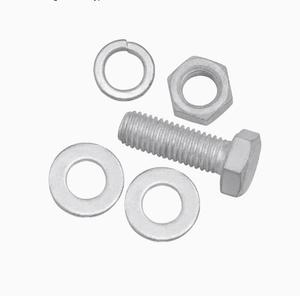
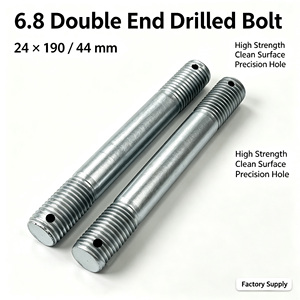
Socket Weld Flanges (SW) manufactured in accordance with ASME B16.5 and DIN EN 1092-1 represent an indispensable piping connection methodology where compact geometry, supreme fatigue resistance, and zero internal leakage under severe thermal fluctuation are paramount. Primarily deployed across nominal bore sizes from NPS 1/2" (DN 15) to NPS 3" (DN 80), socket weld configurations utilize a counter-bored socket that receives the plain-end pipe. This structural design enables optimal internal fluid passage while drastically mitigating the turbulent pressure drops commonly induced by imperfect slip-on inner welds.
Viha Steel & Forging utilizes controlled open and closed-die forging processes to produce continuous grain-flow profiles along the hub and socket transition areas. Unlike flanges machined directly from cheap commercial plate, forged socket weld components provide remarkable impact toughness (tested down to -46°C for ASTM A350 LF2 Class 1) and ultimate tensile properties demanded by international offshore and petrochemical engineering codes.
| Material Specification | Yield Strength (Min, MPa) | Tensile Strength (MPa) | Standard Rating Class | Primary Industrial Utility |
|---|---|---|---|---|
| ASTM A105 Carbon Steel | 250 MPa (36 ksi) | 485 MPa (70 ksi) | Class 150 / 300 / 600 / 1500 | General steam, cooling water, refining process lines |
| ASTM A350 LF2 (Cl. 1) | 250 MPa (36 ksi) | 485 - 655 MPa | Class 300 / 600 / 900 | Low-temperature LNG gas terminals & subsea pipelines |
| ASTM A182 F304/304L | 205 MPa (30 ksi) | 515 MPa (75 ksi) | Class 150 / 300 / 600 | Nitric/organic acid processing, coastal desalination |
| ASTM A182 F316/316L | 205 MPa (30 ksi) | 515 MPa (75 ksi) | Class 150 / 300 / 600 / 1500 | Chloride-laden offshore drilling rigs, marine gas lines |
| ASTM A182 F11 / F22 (Cr-Mo) | 310 MPa (45 ksi) | 485 - 620 MPa | Class 600 / 900 / 1500 / 2500 | High-pressure boiler headers, thermal cracking crackers |
To ensure total connection stability, each socket weld flange is engineered with precise serrated raised face (RF) finishes ranging from 125 to 250 AARH (Ra 3.2 to 6.3 µm) in accordance with ASME B16.5 standards, delivering optimal mechanical bite against spiral wound gaskets (ASME B16.20) equipped with flexible graphite or PTFE fillers.
Vietnam's rapid transition into an advanced global manufacturing powerhouse has catalyzed strict international standards in pressure retaining piping. Socket weld flanges and high-tensile bolting assemblies supplied by Viha Steel & Forging are engineered precisely to combat the harsh equatorial marine atmospheres, high monsoonal humidity, and high-pressure petrochemical parameters native to Vietnamese infrastructure.
Widely utilized across the Dung Quat Refinery (Quang Ngai) and Nghi Son Petrochemical Complex (Thanh Hoa) for small-bore bypass lines, instrumentation sampling networks, catalyst injection feeds, and thermal cracking utilities where leak containment is non-negotiable.
Installed across the Cuu Long Basin, Bach Ho (White Tiger) oilfield, and deepwater exploration modules off Vung Tau. Duplex F51 and 316L socket weld flanges paired with ASTM A193 B8M studs withstand aggressive hypersaline ocean mist and tidal spray.
Integrated into cryogenic storage facilities including the Thi Vai LNG Terminal, as well as Combined Cycle Gas Turbine (CCGT) projects such as Nhon Trach 3 & 4. ASTM A350 LF2 flanges ensure crack arrest during rapid thermal depressurization down to -162°C.
As EPC contractors in Ho Chi Minh City, Hanoi, and Hai Phong harmonize domestic building codes with international project specifications (JIS, ASME, and EN standards), purchasing managers face shifting compliance thresholds.
With Vietnam committing to Net Zero emissions by 2050 at COP26, state-run conglomerates like PVN and EVN enforce strict environmental limits. Socket weld designs are replacing conventional screwed/threaded connections in VOC and hydrocarbon utility lines to permanently eliminate leak paths across valve-manifold interfaces.
Vietnam's Power Development Plan VIII (PDP8) targets colossal offshore wind capacity. Subsea monopile access platforms and hydraulic pitch piping increasingly specify high-integrity ASTM A182 F316L and 2205 Duplex socket weld flanges alongside C5-M marine-grade corrosion-coated bolting.
Vietnamese quality assessment boards (such as QUATEST 3) no longer accept generic broker statements. Engineering procurement teams mandate verifiable EN 10204 Type 3.1 Mill Test Certificates with direct optical emission spectrometry (OES) chemical analysis and Charpy V-notch impact validation.
Headquartered in the manufacturing hub of Mumbai, India, Viha Steel & Forging is a member of the Fastener Manufacturers Association of India (FMAI) and an internationally approved PED (Pressure Equipment Directive 2014/68/EU) manufacturer. We bridge European metallurgical quality with rapid ocean freight transit to Indochina ports.
Every socket weld flange and pressure-containing fitting complies fully with Annex I safety criteria, permitting hassle-free deployment in European and multi-national contractor joint ventures across Vietnam.
Our Mumbai production center houses closed-die drop hammers, state-of-the-art CNC lathes, and non-destructive testing suites (Ultrasonic, Magnetic Particle, Liquid Penetrant) to eradicate internal fissures.
Strategic export consolidation via Nhava Sheva Port (JNPT) provides direct container vessel routes to Cat Lai (Ho Chi Minh City), Hai Phong, and Da Nang in under 12–16 days, supported by comprehensive Form AI FTA documentation.
Direct answers to the most common metallurgical, logistics, and customs inquiries raised by mechanical contractors in Vietnam.
Traceability is the cornerstone of safe process piping. Explore our certified production pathway designed to eliminate manufacturing variances before export.
Raw forged round bars undergo Positive Material Identification (PMI) using stationary optical emission spectrometers to verify chemical composition against ASTM/DIN tables.
Ingots are heated in temperature-monitored furnaces and hot-forged with high-tonnage hammers to maximize grain orientation, improving ductility and impact resistance.
Forgings pass through computer-regulated heat treatment furnaces (Quench & Temper, Normalizing, or Solution Annealing) to relieve mechanical stresses and homogenize microstructure.
Flange faces, bolt-hole circles, and internal sockets are turned on multi-axis CNC machines to achieve tight tolerances (±0.25mm) and standardized serrated surface finishes.
Speak directly with our technical sales engineers in Mumbai. Send your bill of quantities (BOQ), material specifications, or custom drawings for prompt estimation and delivery schedules.
Inquire Now