Precision-Engineered Heavy Industrial Bolting, ASTM/DIN Standard Flanges, and Structural Hardware with Guaranteed Mill Traceability
Manufactured under strict ISO 9001 and PED manufacturing protocols to satisfy demanding structural, pressure vessel, high-temperature, and corrosive pipeline requirements.
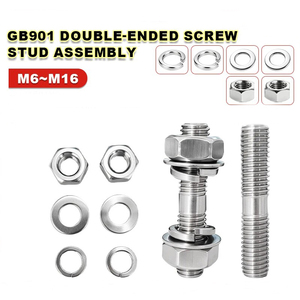
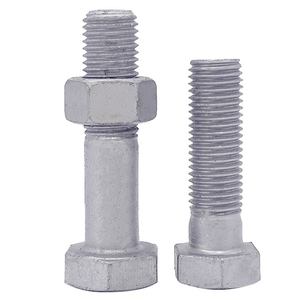
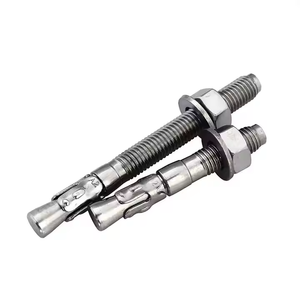
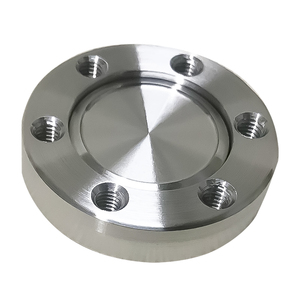
Precision bolted joints are critical path components in petrochemical refineries, subsea pipeline matrices, wind power installations, and heavy civil infrastructure projects.
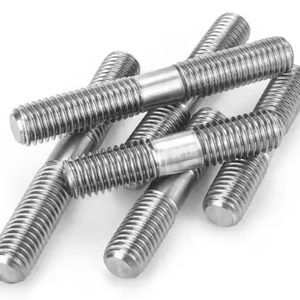
Engineered from normalized, quenched, and tempered AISI 4140, 4142, and 4340 alloy bar stocks. Our ASTM A193 B7 and A320 L7 stud bolts exhibit elevated high-temperature creep resistance (up to 450°C) and documented Charpy V-Notch impact toughness down to -101°C for cryogenic Liquefied Natural Gas (LNG) service valves.
Engineered to ASTM F3125 Grade A325 / A490 and European EN 14399-4 HV standards. Our hot-dip galvanized (HDG) structural bolting sets undergo rigorous wedge tensile testing, rotational capacity verification, and strict torque-tension calibration to prevent brittle fractures under extreme dynamic wind loads on offshore substations and towers.
Beyond carbon and structural alloys, we specialize in solution-annealed austenitic stainless steel (ASTM A193 B8 Class 2, B8M Class 2), precipitation-hardening titanium alloys for aerospace and weight-sensitive motorsport assemblies, and forged ultra-high vacuum ConFlat (CF) rotatable flanges capable of maintaining seals under 10⁻¹⁰ Torr.
Consult our empirical performance matrix when planning international EPC engineering procurements or standard warehouse stocking programs.
| Specification / Grade | Base Material & Treatment | Tensile Strength (Min) | Yield Strength (Min) | Recommended Nut / Washer | Core Industry Applications |
|---|---|---|---|---|---|
| ASTM A193 Grade B7 | AISI 4140/4142 Cr-Mo Steel, Quenched & Tempered | 125 ksi (860 MPa) | 105 ksi (720 MPa) | ASTM A194 Gr. 2H Heavy Hex | Oil & Gas / Pressure Vessels |
| ASTM A320 Grade L7 | Chromium-Molybdenum Steel, Low-Temp Impact Tested | 125 ksi (860 MPa) | 105 ksi (720 MPa) | ASTM A194 Gr. 7 / 7M Heavy Hex | LNG Terminals & Cryogenics (-101°C) |
| ASTM F3125 Grade A325 | Medium Carbon / Boron Alloy, Quenched & Tempered | 120 ksi (830 MPa) | 92 ksi (635 MPa) | ASTM A563 DH / ASTM F436 Type 1 | Bridges, Heavy Towers, Steel Building |
| EN 14399-4 Class 10.9 HV | Chromium-Boron Alloy High-Tensile Steel | 1000 MPa (145 ksi) | 900 MPa (130 ksi) | EN 14399-4 Class 10 Nuts | European High-Speed Rail & Cranes |
| ASTM A193 Grade B8M (Cl. 2) | AISI 316 Stainless Steel, Strain Hardened | 110 ksi (760 MPa) | 95 ksi (655 MPa) | ASTM A194 Gr. 8M Heavy Hex | Marine Chemical & Desalination |
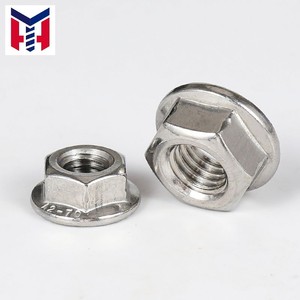
| DIN 6921 Grade 10.9 | Micro-Alloy Structural Steel with Serrated Flange | 1040 MPa | 940 MPa | DIN 6923 Self-Locking Flange Nut | Automotive Engine & Vibration Joints |
Emerging sustainability standards, automated tensioning technologies, and global supply chain reconfigurations are reshaping how international buyers procure wholesale fasteners.
In ultra-high tensile bolts exceeding 1000 MPa tensile strength, electroplating presents catastrophic hydrogen embrittlement risks. Sourcing is rapidly shifting toward non-electrolytic Zinc Flake coatings (such as Geomet, Dacromet, and Magni systems) meeting ISO 10683, providing 1,500+ hours of ASTM B117 salt spray protection without introducing atomic hydrogen to the crystalline boundary.
With the implementation of the EU Carbon Border Adjustment Mechanism (CBAM) and strict Scope 3 ESG audits, Tier-1 EPC contractors require certified mill emissions accounting. Modern alloy steel fastener supply chains integrate Electric Arc Furnace (EAF) production based on traceable steel scrap, accompanied by digital QR heat-code tagging for seamless site QA verification.
Large-scale infrastructure installations like offshore wind turbine jackets and critical high-pressure heat exchangers are demanding embedded piezoelectric sensor bolts. These fasteners enable ultrasonic measurement of genuine axial clamping load in real-time, eliminating friction scatter uncertainties caused by standard torque wrench tightening.
Direct technical and operational answers to address common specification, testing, and shipping questions faced by global procurement officers.
Every batch of raw alloy round bar is tagged with an individual heat number upon arriving at our facility. Complete Spectro-chemical composition, heat-treatment quenching chart logs, and mechanical test specimens (yield, tensile, elongation, and reduction of area) are cataloged under this heat identifier. Every shipment is accompanied by a certified EN 10204 3.1 Mill Test Certificate (MTC) stating the chemical analysis, mechanical performance, and third-party NDT clearance.
ASTM A193 B7 is an alloy steel specification primarily intended for high-temperature, high-pressure piping flanges, valves, and pressure vessels, typically threaded continuously as stud bolts or double-end studs. ASTM A325 (now consolidated under ASTM F3125) specifically designates medium-carbon structural bolts with a shorter thread length designed strictly for structural steel-to-steel joints in buildings and bridges.
For high-tensile alloy fasteners with hardness levels equal to or exceeding 32 HRC (such as Grade 10.9 bolts and ASTM A193 B7), we utilize strict post-plating de-embrittlement baking at 190°C–220°C for a minimum of 4 to 24 hours immediately following acid pickling and electro-galvanizing. Alternatively, we recommend our specialized zinc flake dip-spin coating process, completely avoiding mechanical acid washing and electro-deposition.
Yes. Our CNC machining centers and high-speed cold and hot heading presses manufacture bespoke fasteners up to M100 (4 inches) in diameter. We accommodate custom pitch threads, modified neck radii, left-handed threads, Acme profiles, multi-start threads, and special corrosion barrier platings according to your project blueprints and engineering submittals.
We welcome third-party pre-shipment inspections (PSI) conducted by internationally recognized agencies, including SGS, Bureau Veritas (BV), TÜV Rheinland, DNV GL, and Lloyd's Register. Our dedicated laboratory technicians facilitate witnessing of dimension verification, ultrasonic testing (UT), magnetic particle inspection (MPI), and Charpy impact tests prior to export packing.
Stocked dimensions and standard metric/UNC threaded rods or stud sets ship within 7–10 days. Custom forging and heat-treatment batches require 20–30 days depending on raw material sourcing. All fasteners are packaged in seaworthy, reinforced wooden crates or fumigated export pallets wrapped in moisture-resistant vapor corrosion inhibitor (VCI) shrink wrap for safe intercontinental sea transport.